
Industries
Why manufacturing employees leave and how to understand why
Operators, technicians and supervisors leave for reasons that sit in shifts, skills and supervision. How to ask, read the pattern by shift and act on it.
6 min readRead articleAn extrusion unit runs pipe, film, sheet or profile lines around the clock. A cold start or a grade change eats hours, and the line leader's touch decides how much scrap it makes.

Not sure what you need? Tell us about your business in six short steps and we will come to the first meeting prepared.
Share your requirementsA plastic extrusion unit feeds granules into a heated screw and pushes the melt through a die, giving pipe, blown film, sheet, tube or profile. The product is then cooled, sized, and cut or wound. Many lines run day and night, and every stoppage means hours of off-grade output before a stable run returns. The line leader sets barrel temperatures and screw speed and watches wall thickness, gauge and surface. Operators wind, cut, stack and pack. Buyers are builders, packers, farmers and other makers, ordering by size and grade. See the wider manufacturing HR page as well.
These are the places the people side of this kind of business tends to give way. The rest of this page works through them.
HR here has to work for each of these groups, not only the office. The set-up below is written with all of them in mind.
A new diameter or colour needs a careful restart, and the line leader's skill decides how many metres are scrapped.
Holding gauge on a hot afternoon or clearing a choked die is seldom written down, and an exit hurts for months.
The winder operator cannot walk away for long, so tea breaks, meals and relief get skipped.
Resin quality and a worn die cause scrap too, and operators feel accused of faults that start elsewhere.
Hot barrels, cooling steam and drive noise wear people down, most of all on summer nights.
Line supervisors are promoted on skill, yet nobody taught them to plan a shift or give feedback.
Start with the topics that matter most here: Learning and Development; Compensation, Payroll and Benefits; Career and Succession Management. Then work through the rest. Each topic is written for manufacturing, not in general.
Training planned from need rather than from the calendar.
Salary structure, payroll inputs and a month that closes on time.
Named backups for the roles that cannot be vacant.
How many people, in which roles, by when — and what they will cost.
Structure, reporting lines and who is allowed to decide what.
Requisition to joining, the same way every time.
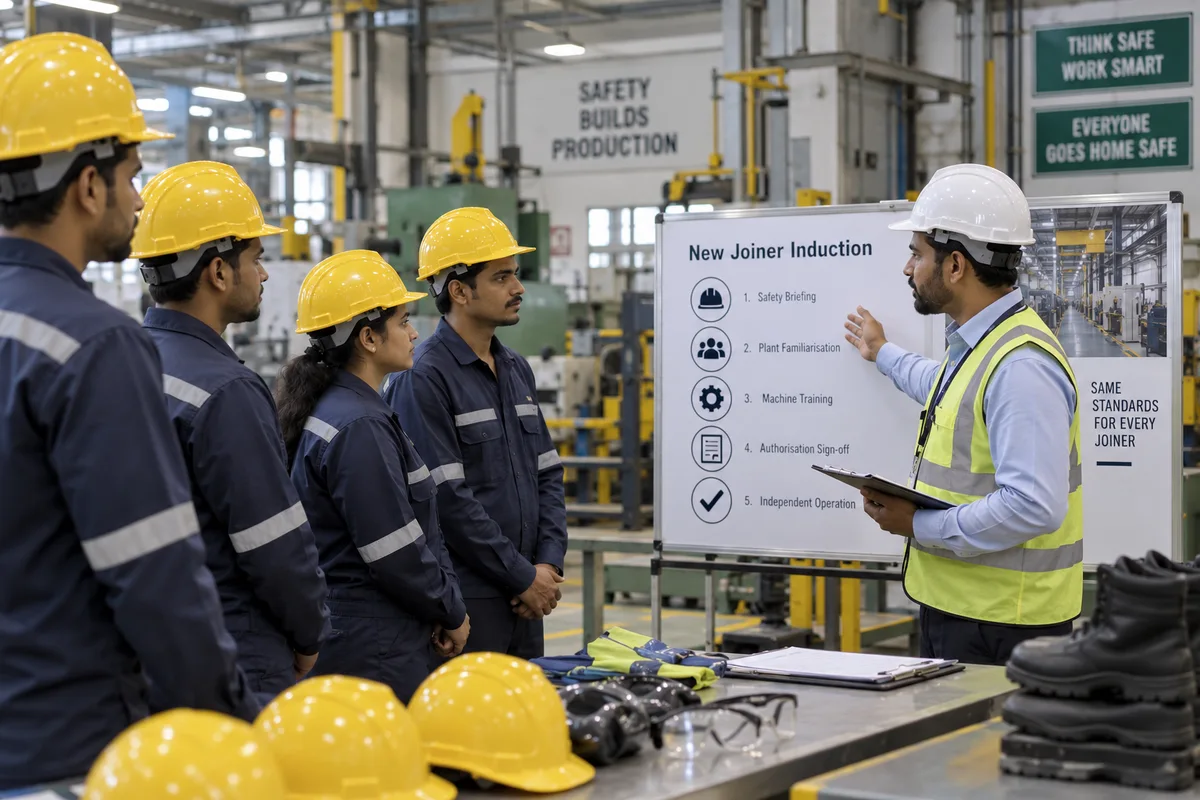
A first day that is the same for the fifth joiner as the first.
Records, attendance, leave and the day-to-day HR that must simply work.
Goals, reviews and ratings that hold up in a conversation.
Communication, recognition and the conditions people actually work in.
Two routes — one for complaints, one for conduct — kept separate.
Policies a manager can apply, and obligations with owners and dates.
Induction, records, incident reporting and follow-through.
Who leaves, when, why — and which of them mattered.
Resignation to relieving letter, in a defined order.
Records that survive people, and approvals that do not queue.
A short monthly pack management actually reads.
An HR function that runs the same way every month.
The pieces a plastic extrusion units business puts in place, in an order that makes each easier. Open any card for the detail.
Steps, temperatures, speeds and warning signs for each product, built by the leader and kept at the line.
What this coversHideSteps, temperatures, speeds and warning signs for each product, built by the leader and kept at the line. Learning and development can host it.
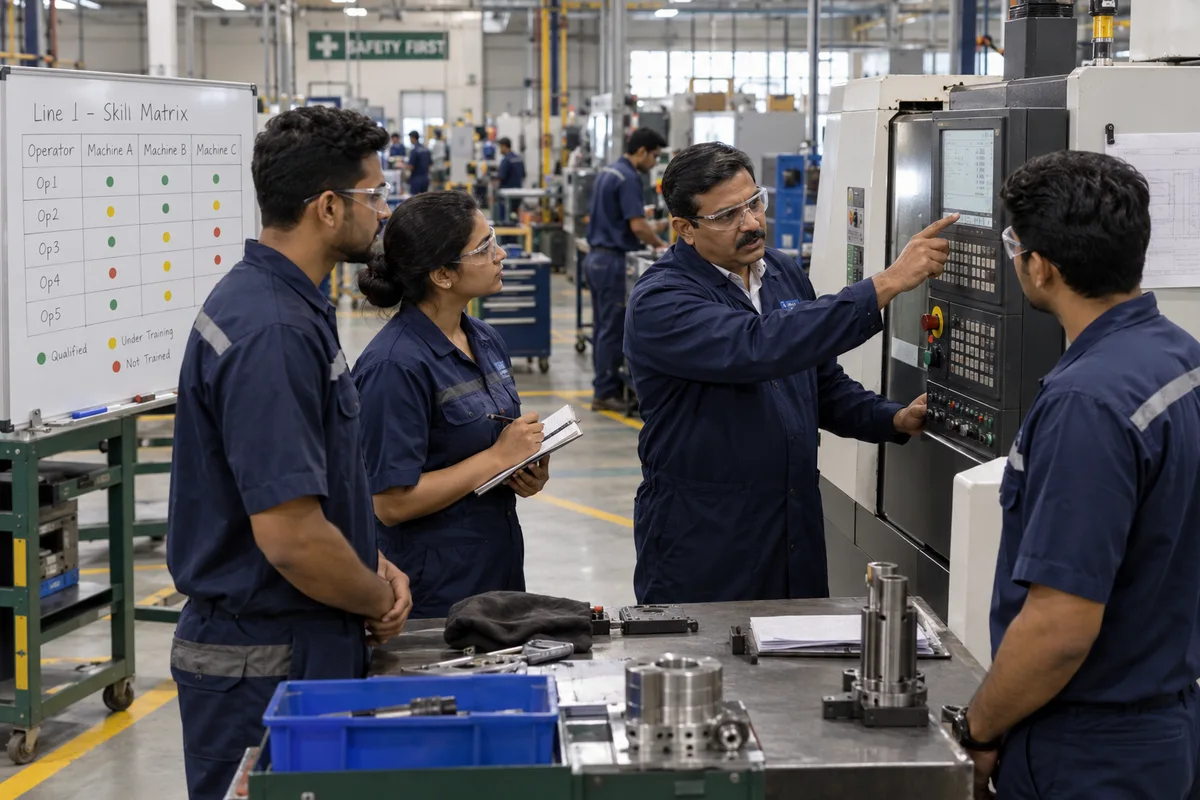
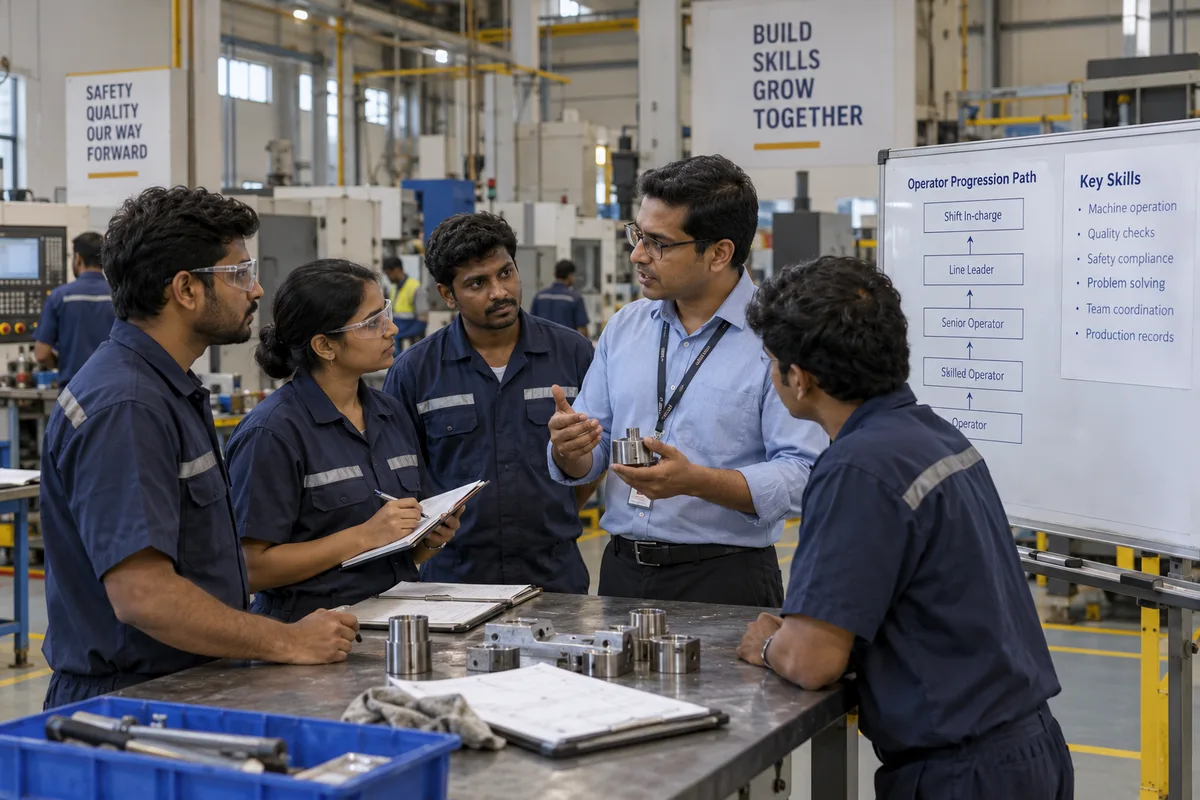
A scale showing what each person can run alone, with a pay step at each level through compensation benchmarking.
What this coversHideA scale showing what each person can run alone, with a pay step at each level through compensation benchmarking.
A named relief operator and a break rota, so nobody is stuck at the winder all shift.
What this coversHideA named relief operator and a break rota, so nobody is stuck at the winder all shift. See attendance, shift and leave.
A monthly sitting of operators, leaders and maintenance, tagging scrap as resin, die wear, setting or handling, so blame turns into fixes.
What this coversHideA monthly sitting of operators, leaders and maintenance, tagging scrap as resin, die wear, setting or handling, so blame turns into fixes.
A short course on shift planning, feedback and handover, drawn from the manager development programme.
What this coversHideA short course on shift planning, feedback and handover, drawn from the manager development programme.
Before changing anything, find out what is true today. These checks take an afternoon and tell you which of the topics above to start with.
Share your requirementsConfirm with a qualified professional. What applies to you depends on your business, your state and your arrangements, and it changes. This page describes practice. It does not state a legal position.
The services below fit this kind of business best. Each starts by recording where you stand, and every later report compares against that. We do not promise outcomes.
Written start-up sheets and a route to line leader, so running knowledge is shared and not carried in one head.
A skill-based grade for winders, extruder operators and line leaders.
Practical training for the operator who has just become a supervisor.
Break, relief and rotation rules for lines that cannot be stopped.
Start with a free conversation, or see the paid HR Diagnostic.
Understand the business, its workforce, current processes and HR challenges.
Find the missing, weak, inconsistent or person-dependent processes.
Create the structure, processes, policies, SOPs, dashboards and systems needed.
Help HR and department managers actually adopt the new system.
Digitise repetitive and approval-based workflows where it is worth doing.
Track hiring, attendance, employee cost, performance, training and attrition.
Strengthen the people-management system continuously, not once.
From the GullyHR blog: one on HR in manufacturing, and one on each of the topics this page points to.
Operators, technicians and supervisors leave for reasons that sit in shifts, skills and supervision. How to ask, read the pattern by shift and act on it.
6 min readRead article
A calendar of courses, a budget spent by March and no record of what any of it changed. What a learning and development process contains when it starts from need rather than from the catalogue.
7 min readRead article
Most salary structures grew one negotiation at a time. How to build grades and bands from what you already pay, without repricing everybody at once.
8 min readRead article
A two-hour exercise that names the roles you could not fill quickly, who could cover them, and what readiness would actually require.
7 min readRead articleMore on the GullyHR blog.
Write the steps with your line leader, train a second person and review every long start-up the same day. Small fixes add up.
Give them a clear grade and pay step, ask them to train others and credit their skill openly. Leaders leave when they feel taken for granted.
Causes are not sorted. A monthly review by cause, including die wear and resin lots, turns blame into repair.
Name a relief operator, fix a break rota and put it on the line board. People work better knowing relief is coming.
Seldom. The machine sets the pace, so a fixed wage with a quality or scrap bonus is usually fairer.
We would ask each line leader about the longest recent start-up, count who can run a line alone and see how scrap is tagged. A practical opening job is a start-up sheet with a grading scale. Once we have talked, scope is agreed on paper.
All 7 business types in plastic manufacturing · Find another business type
Identify payroll leaks, record gaps and hiring bottlenecks in a free first conversation, and leave knowing what to fix first.
Know what you need? Share your requirements in four short steps.
Want the full picture? See the paid HR Diagnostic.
Prefer a quick message? Chat on WhatsApp