
Industries
Why manufacturing employees leave and how to understand why
Operators, technicians and supervisors leave for reasons that sit in shifts, skills and supervision. How to ask, read the pattern by shift and act on it.
6 min readRead articleA bending shop forms flat cut parts into brackets, channels and boxes on CNC press brakes. Good benders are scarce, and an unclear bend sequence can scrap parts that cost real money to cut.

Not sure what you need? Tell us about your business in six short steps and we will come to the first meeting prepared.
Share your requirementsA CNC bending and press brake shop forms flat sheet parts into finished shapes. Parts arrive from laser or punch cutting, or the shop receives blanks from customers. A bender or programmer decides the bend sequence, tools and back gauge positions, then makes a first part and checks angles and lengths. Heavy sheets need two people, and large panels need support. Jobs come in many small batches, so tooling changes happen often. Skill shows in how well a bender reads a drawing, avoids collisions between the part and the machine and corrects spring-back. Few trained benders exist, and many learn by watching others. See also HR for manufacturing.
These are the places the people side of this kind of business tends to give way. The rest of this page works through them.
HR here has to work for each of these groups, not only the office. The set-up below is written with all of them in mind.
Experienced benders are few, and every shop in the area knows who they are.
When a bender leaves, the shop loses the sequence knowledge for repeat parts, and mistakes follow.
Bending large panels needs a helper, and an unreliable helper puts the bender at risk and slows work.
Wrong dies fitted or poorly aligned tools lead to angle errors and marks on parts.
A new sheet batch bends differently, and operators with less experience scrap parts before they adjust.
Fingers near the tool, rushed loading and weak guarding habits lead to injuries, which then keep skilled benders away.
Start with the topics that matter most here: Health, Safety and Wellbeing; Learning and Development; Retention and Attrition Management. Then work through the rest. Each topic is written for manufacturing, not in general.
Induction, records, incident reporting and follow-through.
Training planned from need rather than from the calendar.
Who leaves, when, why — and which of them mattered.
How many people, in which roles, by when — and what they will cost.
Structure, reporting lines and who is allowed to decide what.
Requisition to joining, the same way every time.
A first day that is the same for the fifth joiner as the first.
Records, attendance, leave and the day-to-day HR that must simply work.
Salary structure, payroll inputs and a month that closes on time.
Goals, reviews and ratings that hold up in a conversation.
Named backups for the roles that cannot be vacant.
Communication, recognition and the conditions people actually work in.
Two routes — one for complaints, one for conduct — kept separate.
Policies a manager can apply, and obligations with owners and dates.
Resignation to relieving letter, in a defined order.
Records that survive people, and approvals that do not queue.
A short monthly pack management actually reads.
An HR function that runs the same way every month.
The pieces a CNC bending and press brake shops business puts in place, in an order that makes each easier. Open any card for the detail.
A shared folder with the sequence, tools, angles and notes for every repeat job, so it is not just in one head.
What this coversHideA shared folder with the sequence, tools, angles and notes for every repeat job, so it is not just in one head. The HR documentation process can help structure it.
A short induction on lifting, signals and positions around the machine.
What this coversHideA short induction on lifting, signals and positions around the machine. See health, safety and wellbeing.
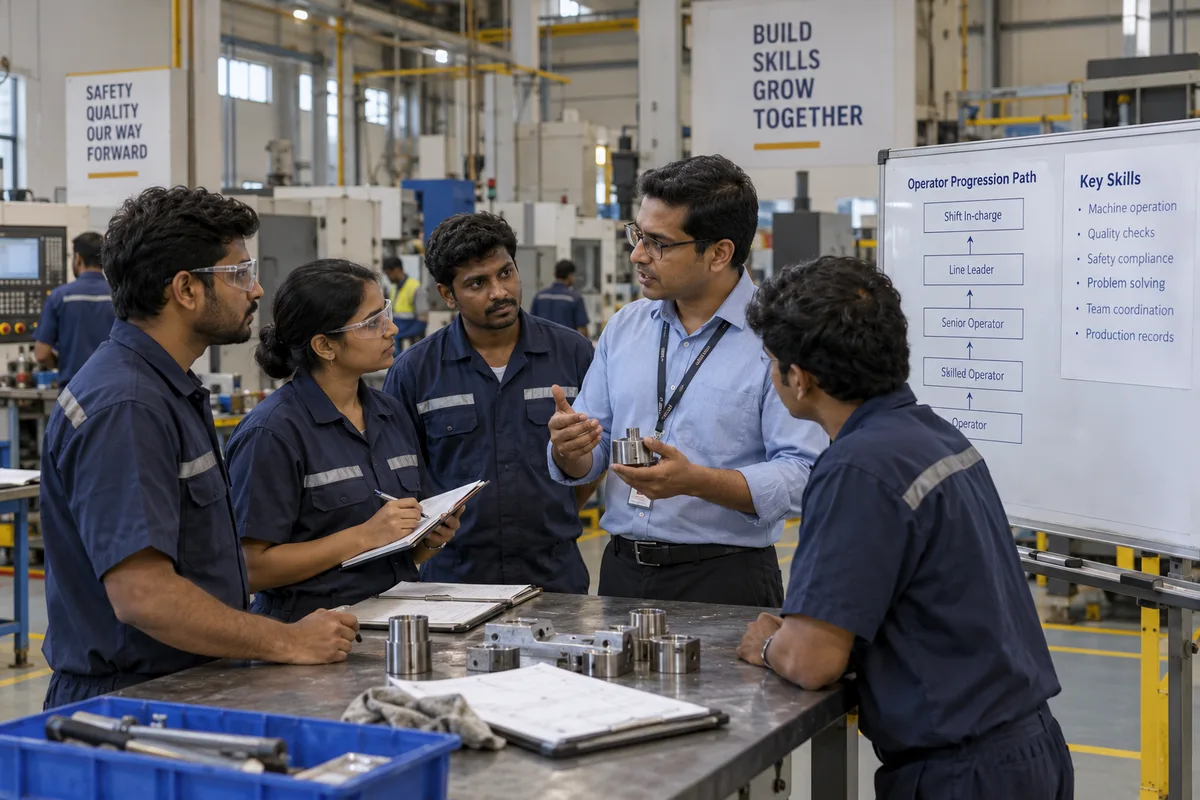
From helper to junior bender to full bender to programmer, each with listed tasks.
What this coversHideFrom helper to junior bender to full bender to programmer, each with listed tasks. Pair it with compensation benchmarking.
A short check of die selection, alignment and first-piece measurement after every tool change.
What this coversHideA short check of die selection, alignment and first-piece measurement after every tool change.
Run a trial piece when a new sheet batch arrives and share results with all benders on the shift.
What this coversHideRun a trial piece when a new sheet batch arrives and share results with all benders on the shift.
Before changing anything, find out what is true today. These checks take an afternoon and tell you which of the topics above to start with.
Share your requirementsConfirm with a qualified professional. What applies to you depends on your business, your state and your arrangements, and it changes. This page describes practice. It does not state a legal position.
The services below fit this kind of business best. Each starts by recording where you stand, and every later report compares against that. We do not promise outcomes.
Guarding habits, two-person handling and hand safety for press brake work.
Helps record bend sequences and job knowledge so repeat jobs survive a resignation.
Grades and pay for benders set against a small, competitive local market.
A route from helper to bender to programmer with skills signed off.
Start with a free conversation, or see the paid HR Diagnostic.
Understand the business, its workforce, current processes and HR challenges.
Find the missing, weak, inconsistent or person-dependent processes.
Create the structure, processes, policies, SOPs, dashboards and systems needed.
Help HR and department managers actually adopt the new system.
Digitise repetitive and approval-based workflows where it is worth doing.
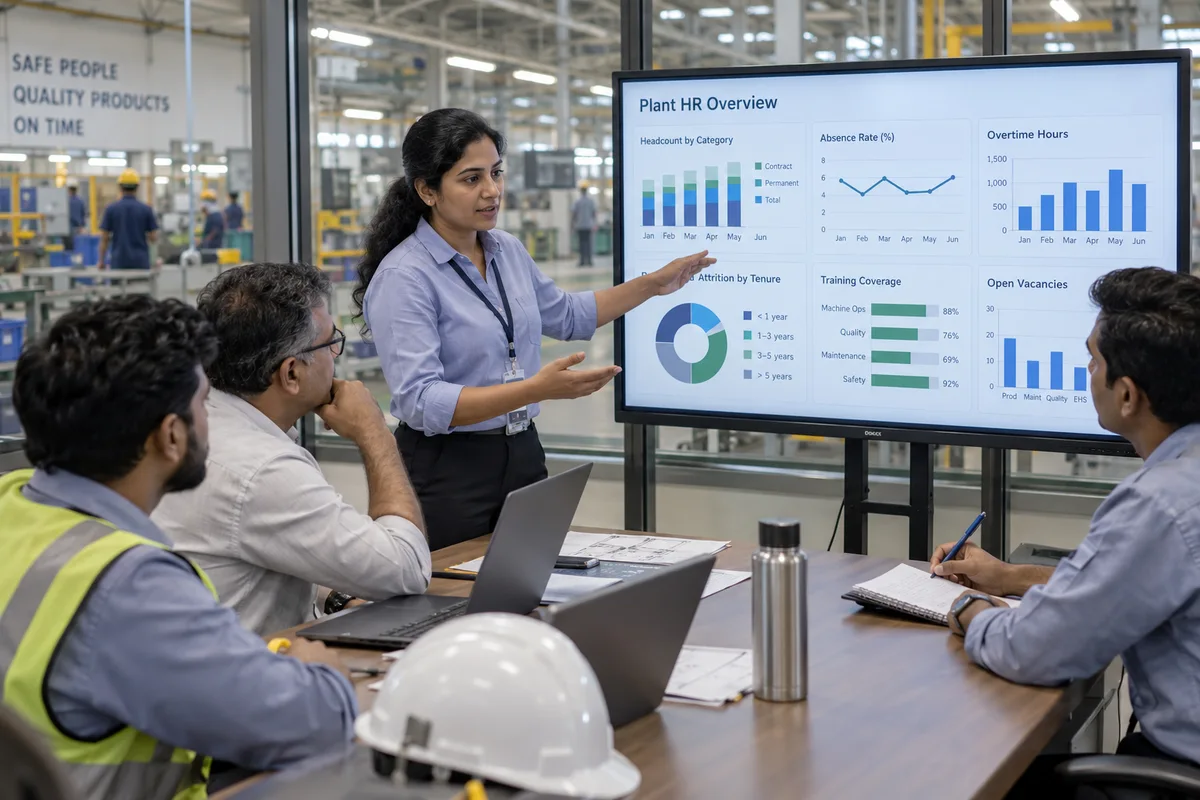
Track hiring, attendance, employee cost, performance, training and attrition.
Strengthen the people-management system continuously, not once.
From the GullyHR blog: one on HR in manufacturing, and one on each of the topics this page points to.
Operators, technicians and supervisors leave for reasons that sit in shifts, skills and supervision. How to ask, read the pattern by shift and act on it.
6 min readRead article
A laminated notice, an annual drill, and an incident register with three entries in two years. What workplace health and safety looks like when it is real.
7 min readRead article
A calendar of courses, a budget spent by March and no record of what any of it changed. What a learning and development process contains when it starts from need rather than from the catalogue.
7 min readRead article
How to spot an unmanageable workload before it becomes an exit or an error, what to look at, how to talk about it and what to change, without guessing.
5 min readRead articleMore on the GullyHR blog.
Begin with helper tasks, move to simple parts under supervision and sign off skills in steps. Allow time for angle correction and spring-back practice.
Give them a grade, fair pay and some say in job planning. Keep an eye on the local market because offers come through colleagues.
Keep guards and light curtains in use, train helpers properly and remove the pressure to rush. Look at near misses weekly.
They keep repeat jobs consistent, speed up set-up and reduce reliance on one person. They also help train juniors faster.
The bender usually knows best on the floor. A planner can set the general approach, and the sequence is recorded after the first successful part.
We would list benders and what each can handle alone, check whether repeat bend sequences are written and review safety records around the machine. A good first piece of work is a bender grade ladder with a sequence library. Scope is agreed in writing afterwards.
All 8 business types in sheet metal and fabrication · Find another business type
Identify payroll leaks, record gaps and hiring bottlenecks in a free first conversation, and leave knowing what to fix first.
Know what you need? Share your requirements in four short steps.
Want the full picture? See the paid HR Diagnostic.
Prefer a quick message? Chat on WhatsApp