
Industries
Why manufacturing employees leave and how to understand why
Operators, technicians and supervisors leave for reasons that sit in shifts, skills and supervision. How to ask, read the pattern by shift and act on it.
6 min readRead articleAerospace CNC shops machine small batches of tight-tolerance parts in titanium, aluminium and steel to customer drawings. The hard part for people is that every job is traceable to one named operator and inspector.

Not sure what you need? Tell us about your business in six short steps and we will come to the first meeting prepared.
Share your requirementsAn aerospace CNC parts maker cuts housings, brackets, fittings and structural pieces from bar, plate and forgings, mostly in small batches against customer drawings and approved process sheets. A job moves from programming and fixture design to set-up, first-piece machining, inspection, deburring, surface treatment through outside vendors and packing with its paperwork. Five-axis and multitasking machines are costly, so they run long hours and shifts, and a single scrapped exotic-alloy part hurts. Operators are trained slowly because the drawing, the programme and the inspection record all have to agree. Orders arrive as repeat schedules with sudden drawing revisions. Programmers, senior setters and inspectors are few and are often approached by rivals. See also HR for manufacturing.
These are the places the people side of this kind of business tends to give way. The rest of this page works through them.
HR here has to work for each of these groups, not only the office. The set-up below is written with all of them in mind.
Proving a five-axis programme for a difficult part takes weeks, and when the person who wrote it leaves, the shop cannot repeat the job with confidence.
Many operators load and unload well but depend on one setter for offsets and tool changes, so a single absence stops a machine.
A correct part with a missing signature or an unreadable batch record may not be accepted, so habits at the bench matter as much as skill.
A revision known in the office but not at the machine produces scrap, and operators are blamed for what was a communication gap.
Machines run unattended or lightly staffed at night while the senior setter has gone home, so small faults grow into scrap.
Inspectors who can read complex drawings and measuring equipment are hard to find, and an offer from a larger plant is enough to lose one.
Start with the topics that matter most here: Learning and Development; Retention and Attrition Management; Compensation, Payroll and Benefits. Then work through the rest. Each topic is written for manufacturing, not in general.
Training planned from need rather than from the calendar.
Who leaves, when, why — and which of them mattered.
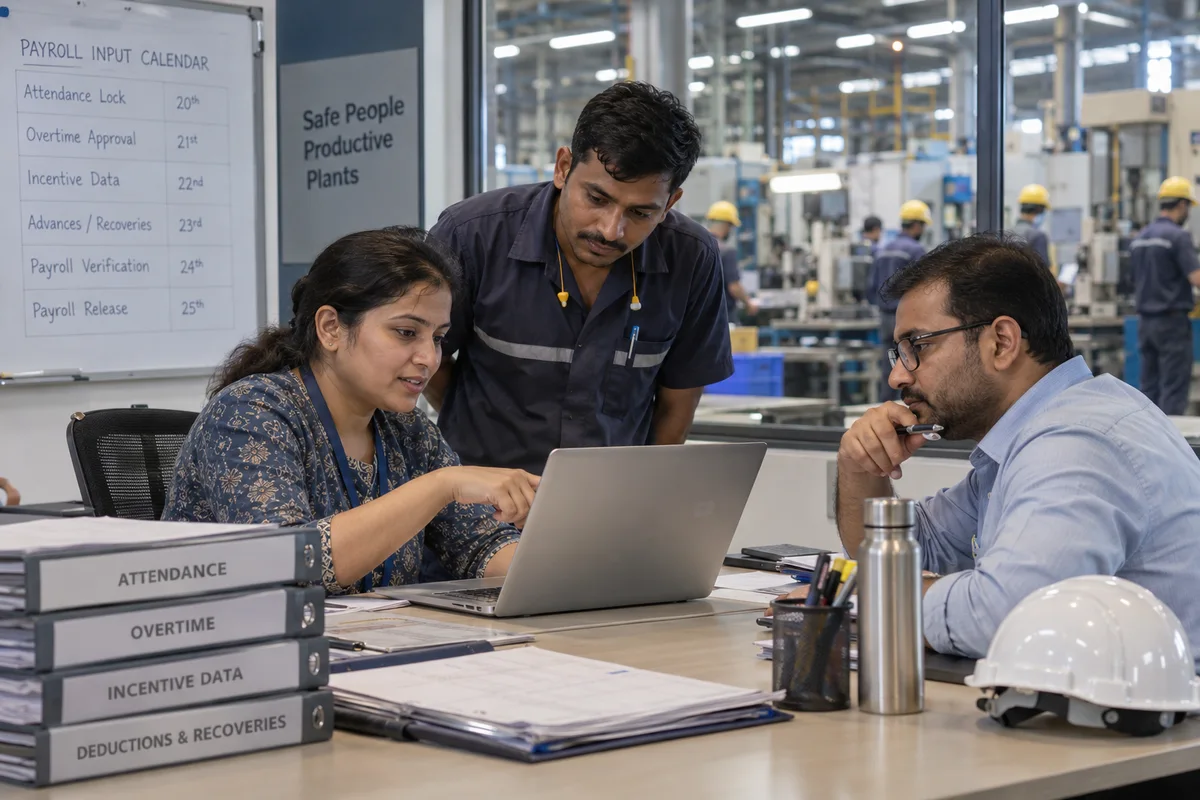
Salary structure, payroll inputs and a month that closes on time.
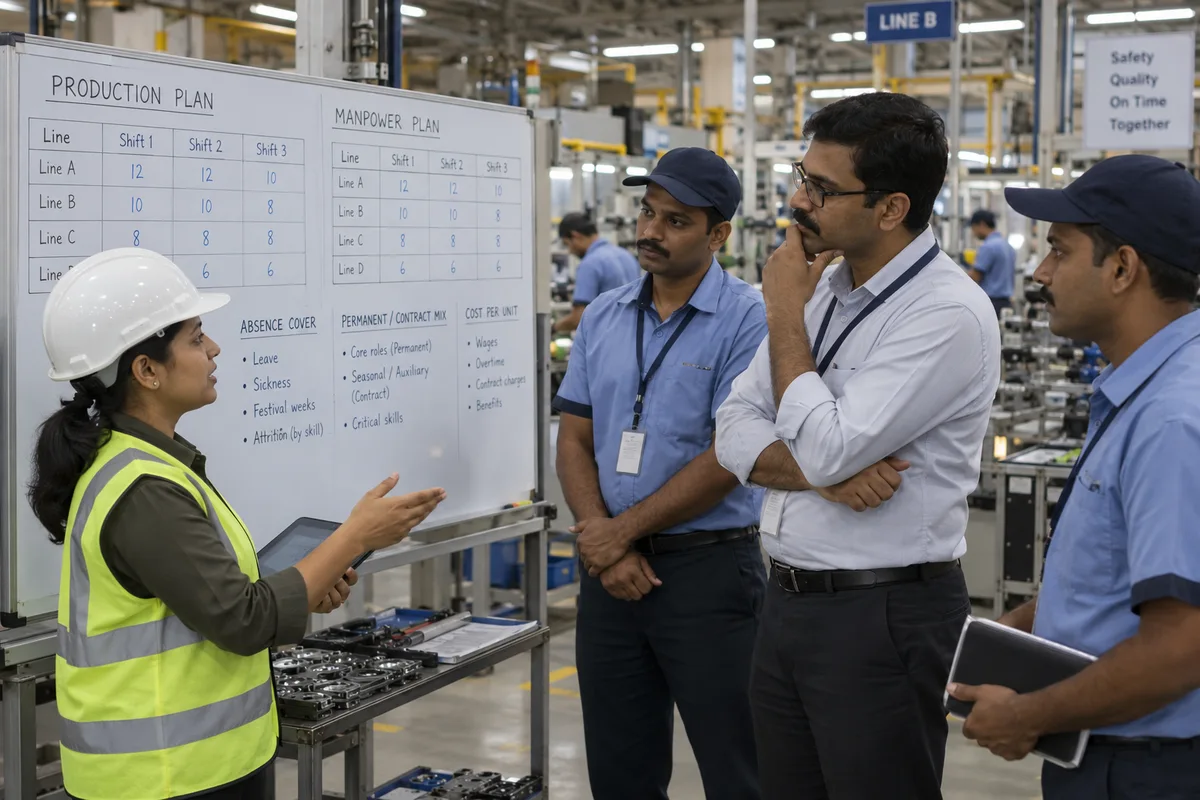
How many people, in which roles, by when — and what they will cost.
Structure, reporting lines and who is allowed to decide what.
Requisition to joining, the same way every time.
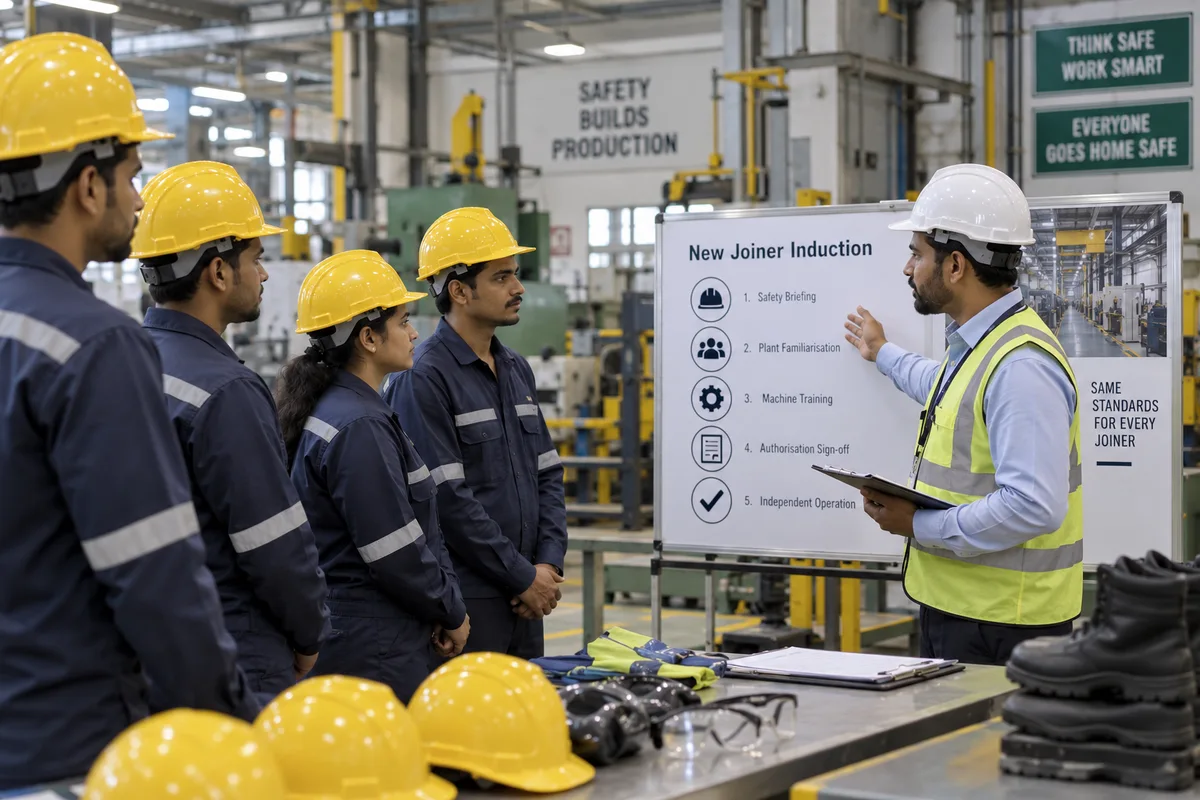
A first day that is the same for the fifth joiner as the first.
Records, attendance, leave and the day-to-day HR that must simply work.
Goals, reviews and ratings that hold up in a conversation.
Named backups for the roles that cannot be vacant.
Communication, recognition and the conditions people actually work in.
Two routes — one for complaints, one for conduct — kept separate.
Policies a manager can apply, and obligations with owners and dates.
Induction, records, incident reporting and follow-through.
Resignation to relieving letter, in a defined order.
Records that survive people, and approvals that do not queue.
A short monthly pack management actually reads.
An HR function that runs the same way every month.
The pieces a aerospace CNC parts makers business puts in place, in an order that makes each easier. Open any card for the detail.
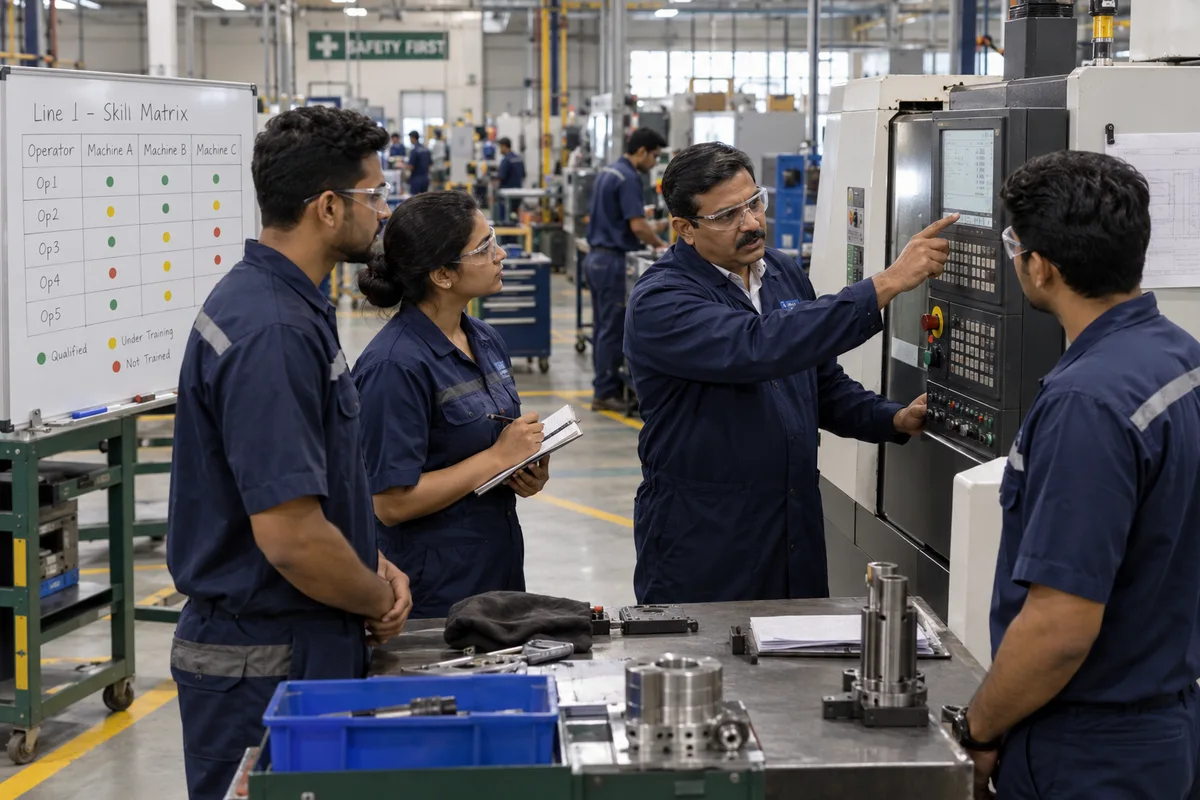
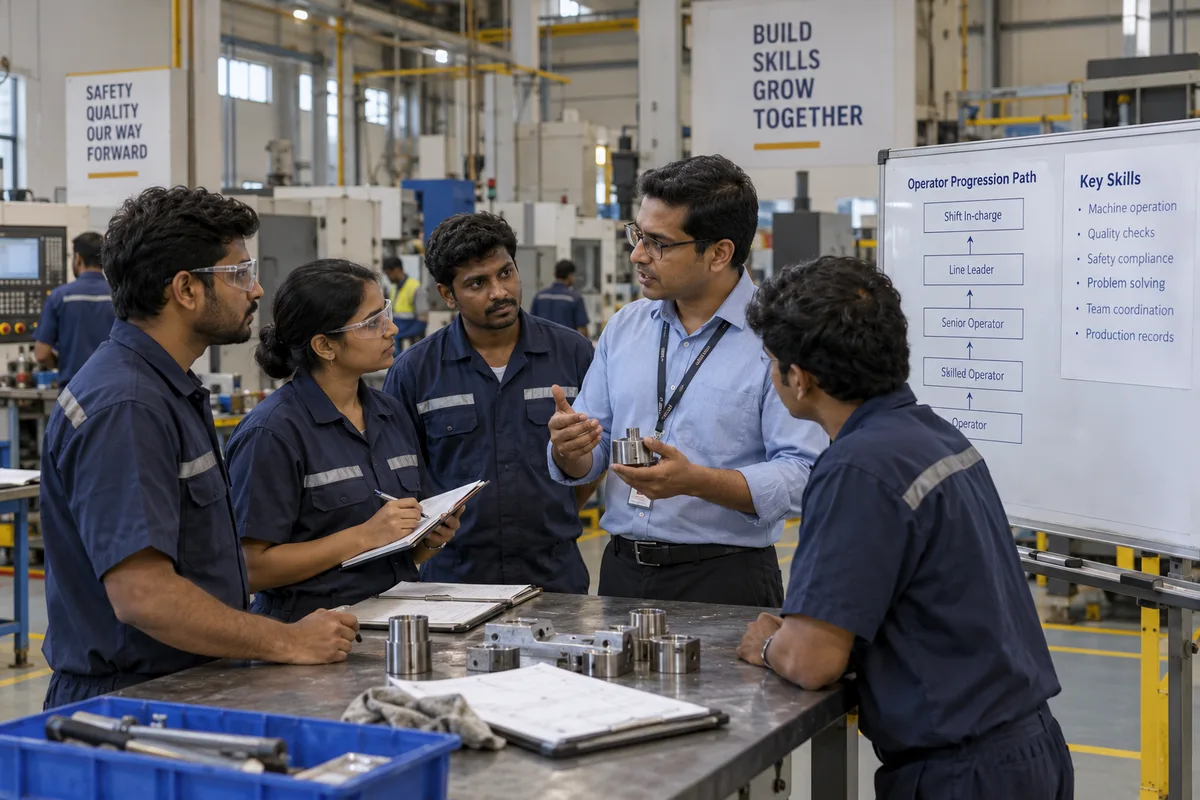
Write levels from loading operator to proving setter to programmer, with the machines and materials each level may handle.
What this coversHideWrite levels from loading operator to proving setter to programmer, with the machines and materials each level may handle. Link it to pay through compensation benchmarking.
Ask each programmer to document the hard jobs and train one understudy per family of parts.
What this coversHideAsk each programmer to document the hard jobs and train one understudy per family of parts. Recognise this in the grade, as the learning and development process can structure.
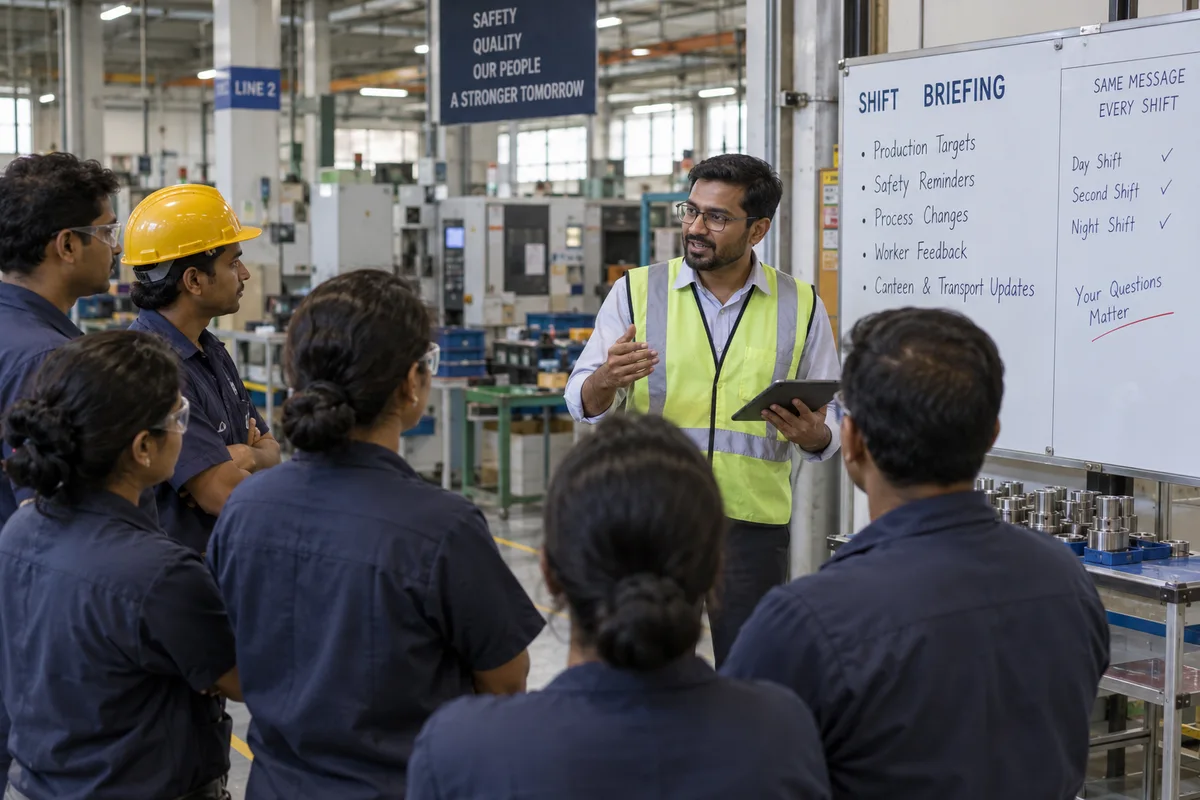
The supervisor confirms at each shift start that the drawing revision at the machine matches the planner's list, and signs for it.
What this coversHideThe supervisor confirms at each shift start that the drawing revision at the machine matches the planner's list, and signs for it. It costs a minute and prevents silent scrap.
Even one setter on site changes what an operator dares to stop.
What this coversHideEven one setter on site changes what an operator dares to stop. Plan it through the attendance, shift and leave process.
New joiners learn why signed records matter and practise on dummy jobs before live work.
What this coversHideNew joiners learn why signed records matter and practise on dummy jobs before live work. The employee onboarding process can hold the checklist.
Before changing anything, find out what is true today. These checks take an afternoon and tell you which of the topics above to start with.
Share your requirementsConfirm with a qualified professional. What applies to you depends on your business, your state and your arrangements, and it changes. This page describes practice. It does not state a legal position.
The services below fit this kind of business best. Each starts by recording where you stand, and every later report compares against that. We do not promise outcomes.
Skill grades and pay for programmers, setters and inspectors set against nearby shops, so the people you cannot replace see a path.
A planned route from operator to setter to programmer, with the hard jobs documented and understudies named.
A hiring process for machinists and inspectors that tests drawing reading and measuring, not only years of experience.
Shift rosters that keep a senior setter and an inspector on every long-running shift.
Start with a free conversation, or see the paid HR Diagnostic.
Understand the business, its workforce, current processes and HR challenges.
Find the missing, weak, inconsistent or person-dependent processes.
Create the structure, processes, policies, SOPs, dashboards and systems needed.
Help HR and department managers actually adopt the new system.
Digitise repetitive and approval-based workflows where it is worth doing.
Track hiring, attendance, employee cost, performance, training and attrition.
Strengthen the people-management system continuously, not once.
From the GullyHR blog: one on HR in manufacturing, and one on each of the topics this page points to.
Operators, technicians and supervisors leave for reasons that sit in shifts, skills and supervision. How to ask, read the pattern by shift and act on it.
6 min readRead article
A calendar of courses, a budget spent by March and no record of what any of it changed. What a learning and development process contains when it starts from need rather than from the catalogue.
7 min readRead article
How to spot an unmanageable workload before it becomes an exit or an error, what to look at, how to talk about it and what to change, without guessing.
5 min readRead article
Most salary structures grew one negotiation at a time. How to build grades and bands from what you already pay, without repricing everybody at once.
8 min readRead articleMore on the GullyHR blog.
Document each hard job in a shared folder, pair him with an understudy on live work, and give the role a clear grade and pay. Retention improves when the person sees recognition, not just a workload.
The drawing, programme, tooling and inspection record all have to line up, and each is learned on real jobs. A written skill ladder with short sign-offs shows trainees and seniors what comes next.
Many shops keep inspectors independent of the production head so a failed part is reported plainly. Whatever you choose, write the reporting line and make sure inspectors are not pressed to pass late jobs.
Choose one capable setter per night shift, give him clear authority to stop a machine, and write down the checks he makes each hour. Pay the extra responsibility visibly.
Only with care. Volume incentives can push operators to rush on costly material. A team incentive tied to right-first-time parts and on-time delivery tends to fit better. Check payment rules with a qualified professional.
We would ask which jobs depend on one programmer, count operators who can set their own offsets, and review a month of scrap against drawing revisions. A good first piece of work is a skill grading ladder for machinists and inspectors. Scope is agreed in writing before work starts.
All 6 business types in aerospace and defence components · Find another business type
Identify payroll leaks, record gaps and hiring bottlenecks in a free first conversation, and leave knowing what to fix first.
Know what you need? Share your requirements in four short steps.
Want the full picture? See the paid HR Diagnostic.
Prefer a quick message? Chat on WhatsApp