
Industries
Why manufacturing employees leave and how to understand why
Operators, technicians and supervisors leave for reasons that sit in shifts, skills and supervision. How to ask, read the pattern by shift and act on it.
6 min readRead articleA PCB shop turns copper-clad laminate into bare boards through dry-film imaging, etching, drilling and plating. Wet lines, fine-track inspection and a handful of process engineers carry more risk than the headcount suggests.

Not sure what you need? Tell us about your business in six short steps and we will come to the first meeting prepared.
Share your requirementsA bare PCB maker works from customer Gerber files, building boards layer by layer. Inner layers are imaged and etched, then laminated into a multilayer stack. Holes are drilled, copper is plated through them, and outer layers are imaged and etched again. Solder mask, surface finish, routing and flying-probe or fixture test come last. Plating tanks and etchers run on acids, alkalis and baths that drift if nobody titrates them. Orders mix quick-turn prototype lots with repeat runs, each with a ship date. The engineer who knows why a bath misbehaves, and the inspector who spots a nick under magnification, are the two people the plant cannot quickly replace. The wider manufacturing hub covers what plants share.
These are the places the people side of this kind of business tends to give way. The rest of this page works through them.
HR here has to work for each of these groups, not only the office. The set-up below is written with all of them in mind.
A copper bath dosed wrongly or a skipped titration on the plating line can scrap dozens of panels, and the cause is often a tired operator.
Etchers and plating tanks call for aprons, face shields and a working eye-wash station, yet the gear is the first thing skipped when the line is behind.
Replenishment rules, tank limits and fixes for odd defects such as voids or undercut sit with one or two engineers. When they are on leave, nobody else can read the line.
Inspectors checking narrow tracks and microvias for hours miss faults late in the shift, and the customer's incoming check finds them.
Urgent prototype panels jump the queue, so lines are reset often and operators work against the clock while repeat orders wait.
Exposure rooms need lint-free clothing and tidy handling of artwork and film. New helpers copy the shortcuts of the shift before them.
Start with the topics that matter most here: Health, Safety and Wellbeing; Learning and Development; Organisation Design. Then work through the rest. Each topic is written for manufacturing, not in general.
Induction, records, incident reporting and follow-through.
Training planned from need rather than from the calendar.
Structure, reporting lines and who is allowed to decide what.
How many people, in which roles, by when — and what they will cost.
Requisition to joining, the same way every time.
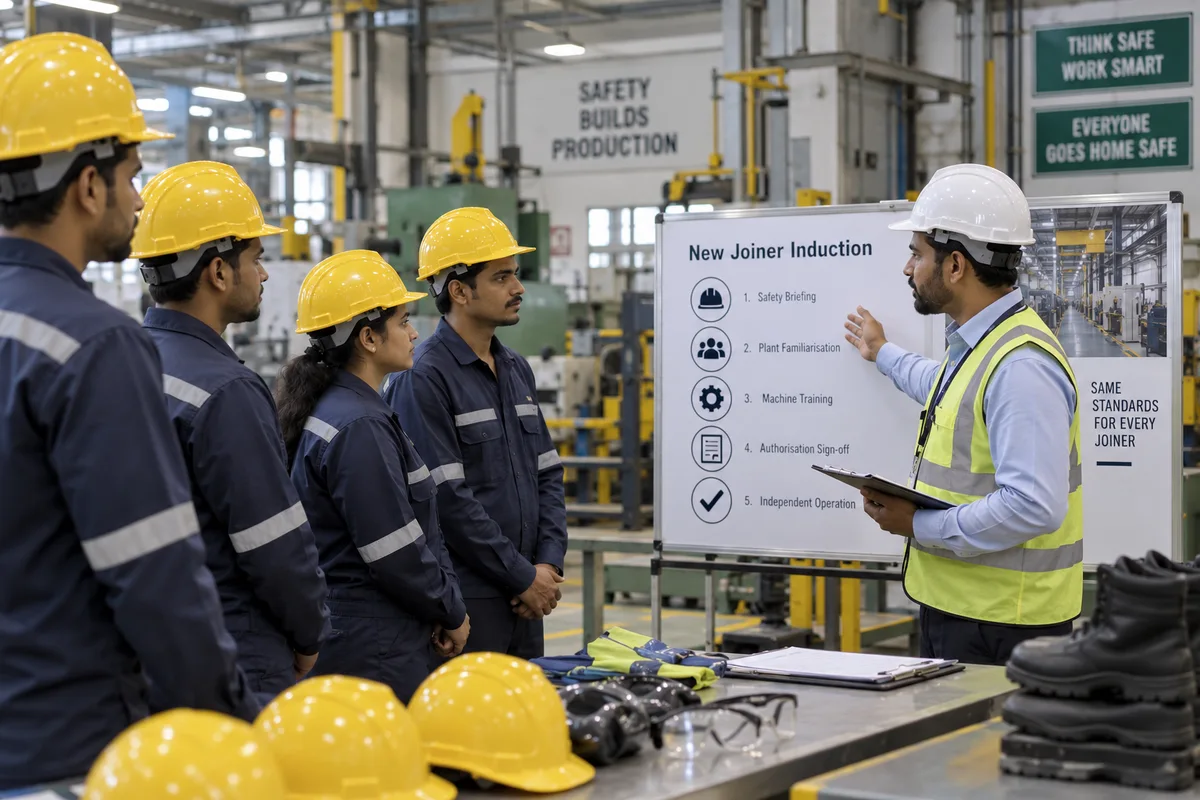
A first day that is the same for the fifth joiner as the first.
Records, attendance, leave and the day-to-day HR that must simply work.
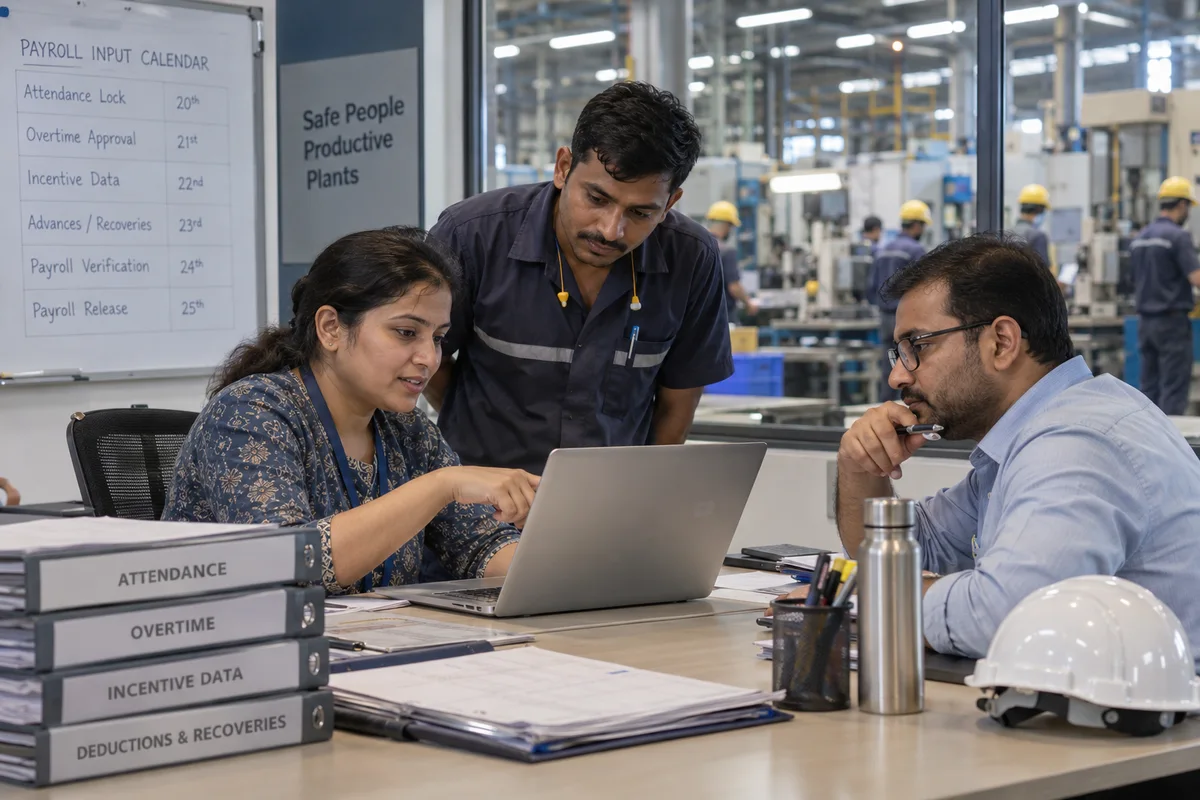
Salary structure, payroll inputs and a month that closes on time.
Goals, reviews and ratings that hold up in a conversation.
Named backups for the roles that cannot be vacant.
Communication, recognition and the conditions people actually work in.
Two routes — one for complaints, one for conduct — kept separate.
Policies a manager can apply, and obligations with owners and dates.
Who leaves, when, why — and which of them mattered.
Resignation to relieving letter, in a defined order.
Records that survive people, and approvals that do not queue.
A short monthly pack management actually reads.
An HR function that runs the same way every month.
The pieces a PCB manufacturers business puts in place, in an order that makes each easier. Open any card for the detail.
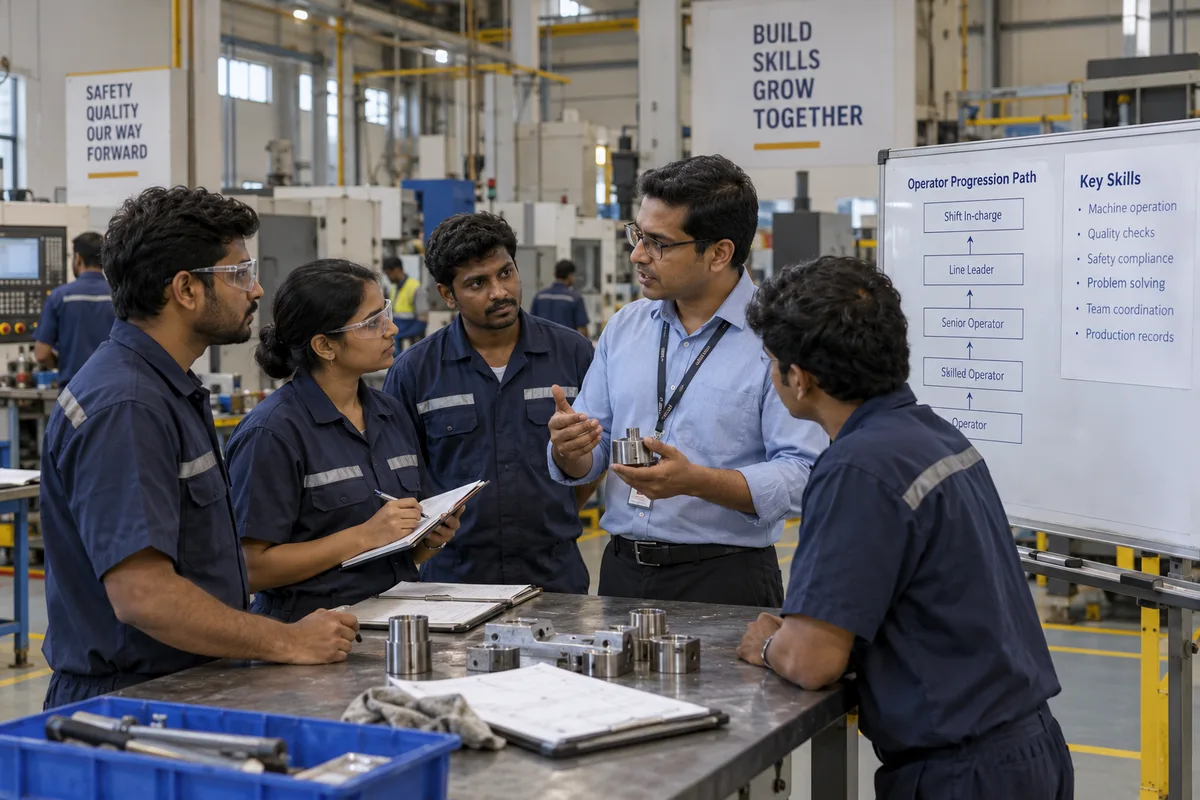
From watching bath additions, to topping up, to running the etcher or plater alone, with a senior signing each rung.
What this coversHideFrom watching bath additions, to topping up, to running the etcher or plater alone, with a senior signing each rung. Build it with sign-off ladders that keep a record.
Aprons, shields, eye wash and spill kit confirmed before the first panel enters, noted on a short sheet.
What this coversHideAprons, shields, eye wash and spill kit confirmed before the first panel enters, noted on a short sheet. The safety and wellbeing work sets the routine.
A shared file of tank limits, adjustment rules and known defect causes, written by the engineer and read through by a second person who has to run the tank from it.
What this coversHideA shared file of tank limits, adjustment rules and known defect causes, written by the engineer and read through by a second person who has to run the tank from it.
Short inspection stints between breaks and other tasks, plus a simple count of defects caught per inspector.
What this coversHideShort inspection stints between breaks and other tasks, plus a simple count of defects caught per inspector. Shift and break patterns fix the rhythm.
A fixed slot each day for quick-turn lots, agreed with sales, so a rush order stops rewriting the plan for the whole shift.
What this coversHideA fixed slot each day for quick-turn lots, agreed with sales, so a rush order stops rewriting the plan for the whole shift.
Before changing anything, find out what is true today. These checks take an afternoon and tell you which of the topics above to start with.
Share your requirementsConfirm with a qualified professional. What applies to you depends on your business, your state and your arrangements, and it changes. This page describes practice. It does not state a legal position.
The services below fit this kind of business best. Each starts by recording where you stand, and every later report compares against that. We do not promise outcomes.
Chemical handling routines and protective gear habits for etchers, strippers and plating tanks.
Sign-off ladders that grow line operators and inspectors from your own helpers.
Shift patterns and breaks that suit continuous wet lines and long inspection stints.
Clear roles for imaging, plating, drilling and inspection, and for the engineers above them.
Start with a free conversation, or see the paid HR Diagnostic.
Understand the business, its workforce, current processes and HR challenges.
Find the missing, weak, inconsistent or person-dependent processes.
Create the structure, processes, policies, SOPs, dashboards and systems needed.
Help HR and department managers actually adopt the new system.
Digitise repetitive and approval-based workflows where it is worth doing.
Track hiring, attendance, employee cost, performance, training and attrition.
Strengthen the people-management system continuously, not once.
From the GullyHR blog: one on HR in manufacturing, and one on each of the topics this page points to.
Operators, technicians and supervisors leave for reasons that sit in shifts, skills and supervision. How to ask, read the pattern by shift and act on it.
6 min readRead article
A laminated notice, an annual drill, and an incident register with three entries in two years. What workplace health and safety looks like when it is real.
7 min readRead article
A calendar of courses, a budget spent by March and no record of what any of it changed. What a learning and development process contains when it starts from need rather than from the catalogue.
7 min readRead article
A flat structure works until the founder becomes the only route to a decision. How to tell when you have passed that point, and how to redesign without a reorganisation.
8 min readRead articleMore on the GullyHR blog.
Put a sign-off ladder in place so nobody runs a tank alone before a senior has checked them, and keep a short bath-check log. Study each scrapped lot for the cause, not the culprit.
Give the role its own grade and pay, ask them about new tanks and drills before you buy, and have someone learn their recipes. Compare pay with nearby fabrication plants.
Shorter stints, rotation onto other tasks and proper lighting at the bench. Show inspectors what escaped to the customer, so accuracy feels connected to something.
Pair each with a senior for the first weeks, show the gear and eye wash on day one, and watch their handling before they work a line alone.
Hold a daily prototype window, tell sales what it can carry, and note what each rush pushed back. You then argue from facts when a customer pushes.
First question: who can run each wet line alone, go through the latest scrap event, and look at the chemical safety check. Early output could be a sign-off ladder for line operators and a written bath-recipe file from your engineers, with the work scope put in writing for your approval after we talk.
All 8 business types in electronics and embedded systems · Find another business type
Identify payroll leaks, record gaps and hiring bottlenecks in a free first conversation, and leave knowing what to fix first.
Know what you need? Share your requirements in four short steps.
Want the full picture? See the paid HR Diagnostic.
Prefer a quick message? Chat on WhatsApp