
Industries
Why manufacturing employees leave and how to understand why
Operators, technicians and supervisors leave for reasons that sit in shifts, skills and supervision. How to ask, read the pattern by shift and act on it.
6 min readRead articleA turning shop runs CNC lathes that make round parts in batches, often for the same customers month after month. The hard part is that a few setters know the machines and the rest only load and unload.

Not sure what you need? Tell us about your business in six short steps and we will come to the first meeting prepared.
Share your requirementsA CNC turning shop cuts shafts, pins, bushes, flanges and fasteners from bar stock or forgings on CNC lathes, some with sub-spindles and bar feeders. Orders arrive as customer drawings with a monthly schedule, and batches are repeated, so the same job returns every few weeks. A setter loads the program, fits the tools, sets offsets and proves the first piece. Operators then load, measure with gauges and micrometers and keep the cycle going. Many shops run two or three shifts to keep the spindles busy. Setters are scarce, operators are often trained on the floor, and the first-piece approval can sit with one person. Night shifts have the least supervision. See also HR for manufacturing.
These are the places the people side of this kind of business tends to give way. The rest of this page works through them.
HR here has to work for each of these groups, not only the office. The set-up below is written with all of them in mind.
Operators run the machine well once it is set, but a changeover waits for one setter, and his absence stops the line.
A setter tunes an offset to hold a size and the next shift repeats the problem because the reason was never written down.
Fewer experienced hands are on at night, so out-of-tolerance parts can run for hours before anyone gauges them.
A helper who loads parts for two years has no clear route to operating or setting, so the ambitious ones move to another shop.
Targets per shift reward speed, and gauge checks at fixed intervals get skipped when the count is behind.
A customer pauses releases and then asks for a month's quantity in a fortnight, which pushes overtime and absence.
Start with the topics that matter most here: Learning and Development; Retention and Attrition Management; Onboarding and Probation. Then work through the rest. Each topic is written for manufacturing, not in general.
Training planned from need rather than from the calendar.
Who leaves, when, why — and which of them mattered.
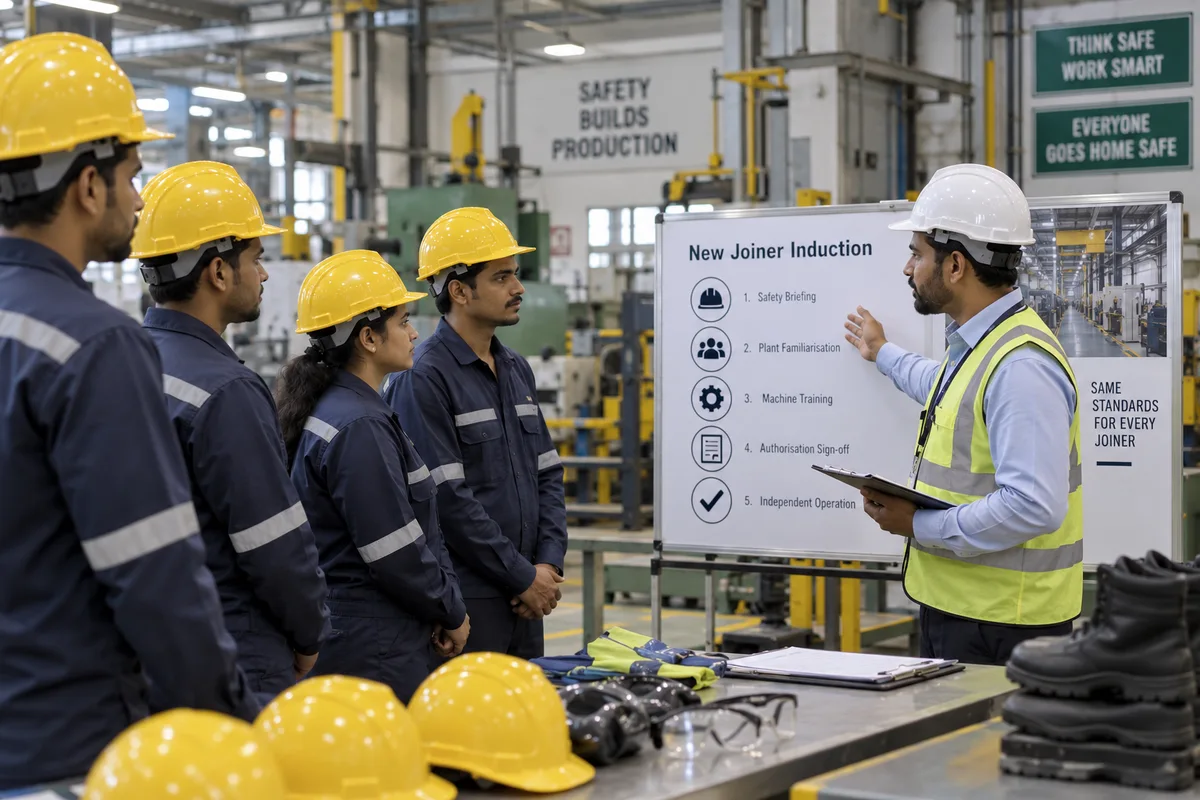
A first day that is the same for the fifth joiner as the first.
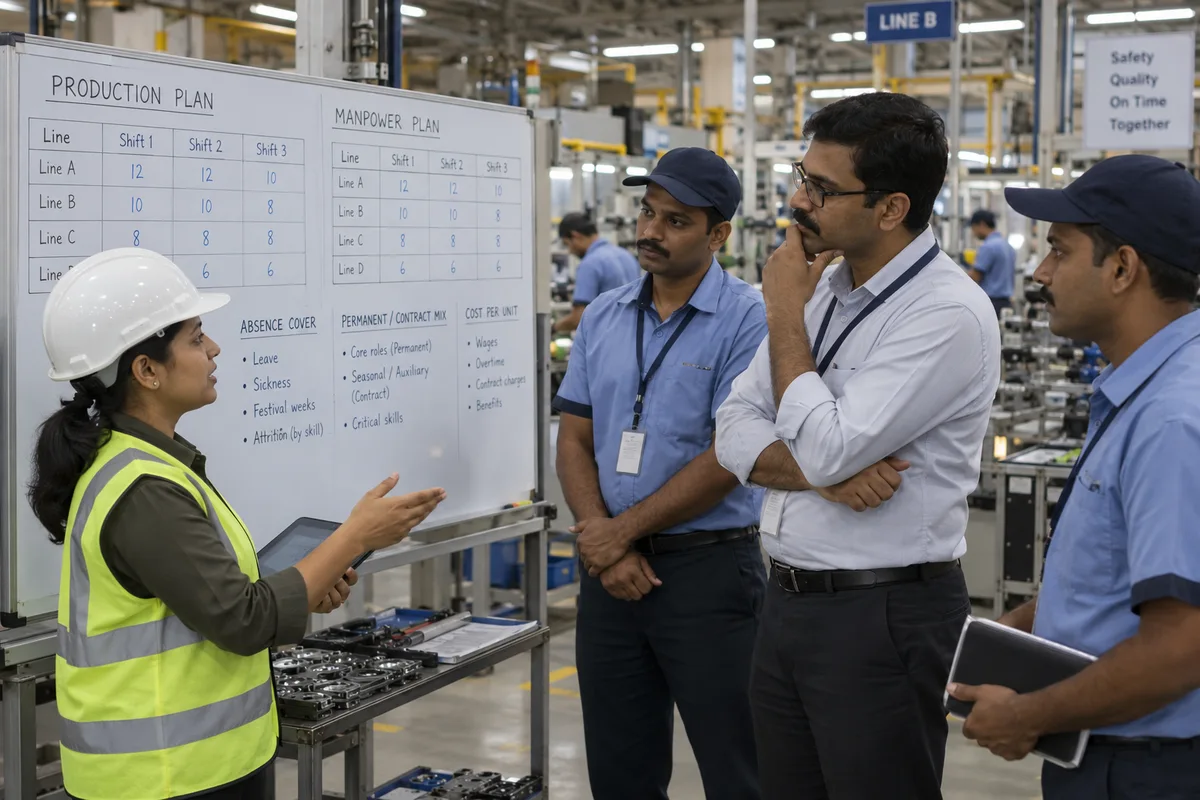
How many people, in which roles, by when — and what they will cost.
Structure, reporting lines and who is allowed to decide what.
Requisition to joining, the same way every time.
Records, attendance, leave and the day-to-day HR that must simply work.
Salary structure, payroll inputs and a month that closes on time.
Goals, reviews and ratings that hold up in a conversation.
Named backups for the roles that cannot be vacant.
Communication, recognition and the conditions people actually work in.
Two routes — one for complaints, one for conduct — kept separate.
Policies a manager can apply, and obligations with owners and dates.
Induction, records, incident reporting and follow-through.
Resignation to relieving letter, in a defined order.
Records that survive people, and approvals that do not queue.
A short monthly pack management actually reads.
An HR function that runs the same way every month.
The pieces a CNC turning shops business puts in place, in an order that makes each easier. Open any card for the detail.
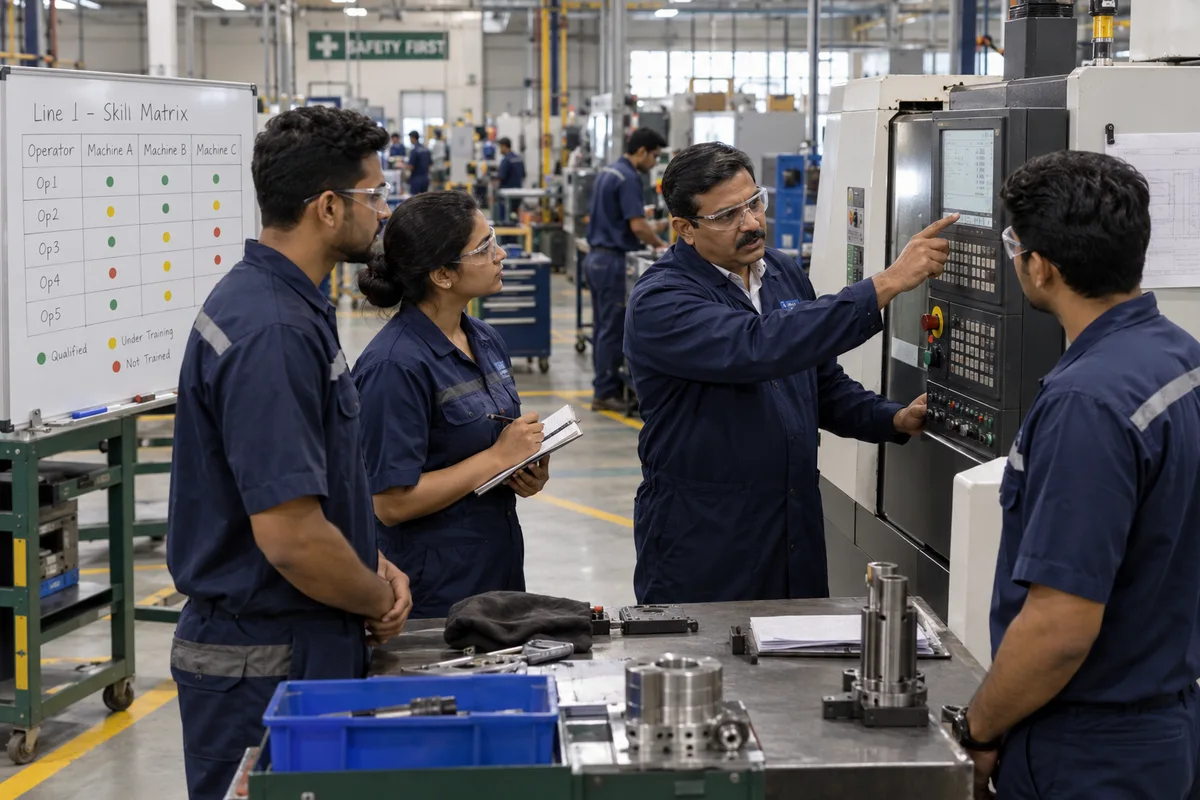
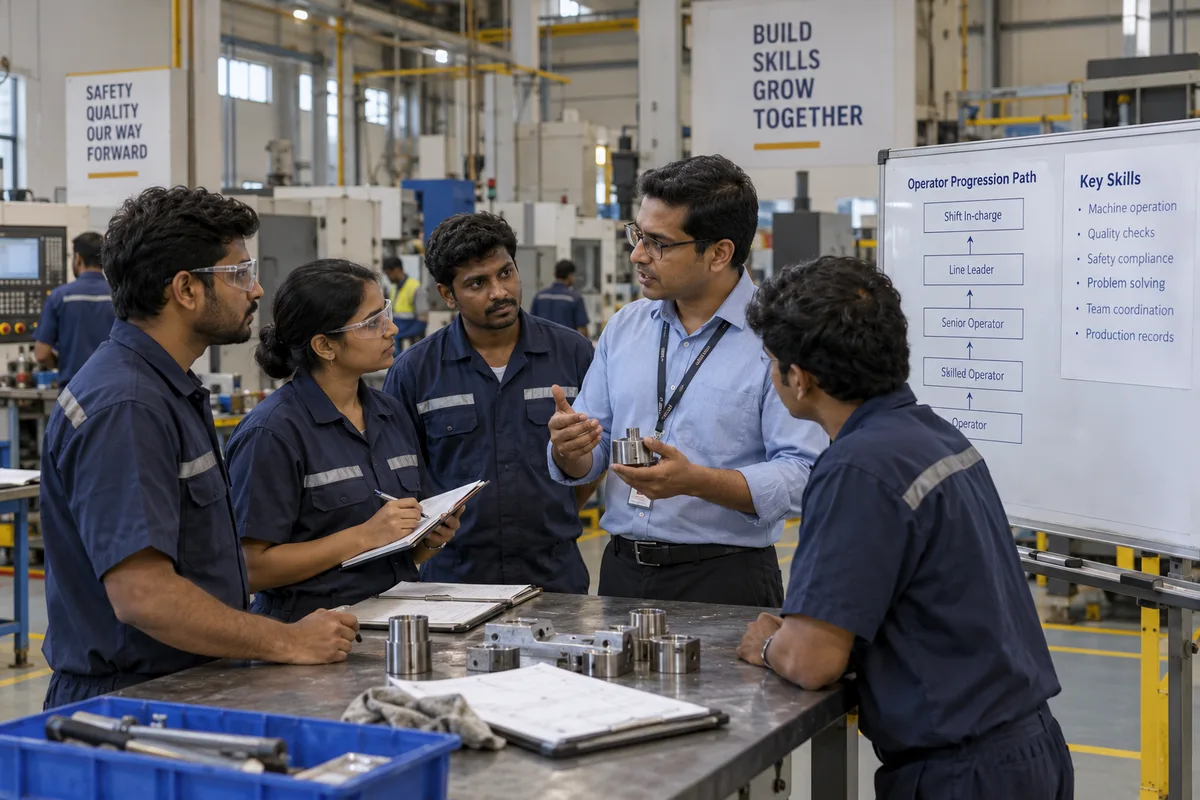
A ladder from loader to operator to setter to programmer, each with listed tasks, such as changing inserts, setting offsets or proving a first piece.
What this coversHideA ladder from loader to operator to setter to programmer, each with listed tasks, such as changing inserts, setting offsets or proving a first piece. Link pay to it using compensation benchmarking.
A simple sheet filled at every changeover with tools used, offsets changed and the reason, so the next shift starts from facts.
What this coversHideA simple sheet filled at every changeover with tools used, offsets changed and the reason, so the next shift starts from facts. Include it in the handover and shift process.
Choose two operators, give them a short list of setter tasks to learn under the senior setter, and sign them off task by task.
What this coversHideChoose two operators, give them a short list of setter tasks to learn under the senior setter, and sign them off task by task. Support it with a learning and development plan.
Write the check interval into the shift routine and have the supervisor sign the sheet.
What this coversHideWrite the check interval into the shift routine and have the supervisor sign the sheet. Pay targets then count checked pieces.
Name a senior operator as night lead with a clear call-out rule for the setter.
What this coversHideName a senior operator as night lead with a clear call-out rule for the setter. Review how shift allocation and leave leaves that shift covered.
Before changing anything, find out what is true today. These checks take an afternoon and tell you which of the topics above to start with.
Share your requirementsConfirm with a qualified professional. What applies to you depends on your business, your state and your arrangements, and it changes. This page describes practice. It does not state a legal position.
The services below fit this kind of business best. Each starts by recording where you stand, and every later report compares against that. We do not promise outcomes.
A structured route from loader to setter, so skill is built inside the shop, not hired at a premium.
Shift rosters, night cover and handover rules that keep experienced hands across all spindles.
Grades and pay for setters and operators set against nearby machine shops.
Looks at why operators and setters leave, and what keeps the ones you cannot replace.
Start with a free conversation, or see the paid HR Diagnostic.
Understand the business, its workforce, current processes and HR challenges.
Find the missing, weak, inconsistent or person-dependent processes.
Create the structure, processes, policies, SOPs, dashboards and systems needed.
Help HR and department managers actually adopt the new system.
Digitise repetitive and approval-based workflows where it is worth doing.
Track hiring, attendance, employee cost, performance, training and attrition.
Strengthen the people-management system continuously, not once.
From the GullyHR blog: one on HR in manufacturing, and one on each of the topics this page points to.
Operators, technicians and supervisors leave for reasons that sit in shifts, skills and supervision. How to ask, read the pattern by shift and act on it.
6 min readRead article
A calendar of courses, a budget spent by March and no record of what any of it changed. What a learning and development process contains when it starts from need rather than from the catalogue.
7 min readRead article
How to spot an unmanageable workload before it becomes an exit or an error, what to look at, how to talk about it and what to change, without guessing.
5 min readRead article
A practical joining checklist covering documents, assets, system access and statutory enrolments, with owners and timings, so nobody's first salary is wrong.
8 min readRead articleMore on the GullyHR blog.
Give them a distinct grade and pay, a say in which jobs are taken, and a part in training others. A setter who sees a path usually stays longer than one who is treated like any operator.
Either can work. Per-piece pay needs a gauge check and a rule that only passed parts count. Fixed pay needs a clear output expectation so that targets do not slip.
Pick a few, list the setter tasks in order, and have the senior setter sign each task off on real jobs. Start with insert changes and offset correction before programming.
Name one capable night lead, give a written call-out rule for quality or breakdown problems, and have the day setter review the night log each morning.
Look at the pattern first, by day and by person. Roster planning, a small attendance reward and a conversation with repeat cases usually help more than blanket warnings.
We would ask who can set each lathe, look at last month's rejections by shift, and check whether changeover knowledge is written down. A good first piece of work is a skill grade for loaders, operators and setters. Scope is agreed in writing afterwards.
All 9 business types in CNC machining and precision engineering · Find another business type
Identify payroll leaks, record gaps and hiring bottlenecks in a free first conversation, and leave knowing what to fix first.
Know what you need? Share your requirements in four short steps.
Want the full picture? See the paid HR Diagnostic.
Prefer a quick message? Chat on WhatsApp