
Industries
Why manufacturing employees leave and how to understand why
Operators, technicians and supervisors leave for reasons that sit in shifts, skills and supervision. How to ask, read the pattern by shift and act on it.
6 min readRead articleA VMC unit runs vertical machining centres on repeat batches, often as job work for larger firms. Output depends on keeping every spindle loaded across shifts with a thin bench of setters.

Not sure what you need? Tell us about your business in six short steps and we will come to the first meeting prepared.
Share your requirementsA VMC machining unit has vertical machining centres, sometimes with tombstones, rotary tables or pallet changers, and cuts parts in medium batches for automotive, pump, valve and general engineering customers. Much of the work is job work: the customer sends castings or forgings with a drawing, and the unit machines and returns them. A setter prepares the fixture and program, operators load and unload and an inspector checks key dimensions at set intervals. Three shifts are common. The business grows by adding machines, but each new machine needs another setter and two operators, and those are the scarce people. Customer releases arrive in waves. See also HR for manufacturing.
These are the places the people side of this kind of business tends to give way. The rest of this page works through them.
HR here has to work for each of these groups, not only the office. The set-up below is written with all of them in mind.
Machines can be bought faster than setters can be trained, so new spindles sit part-loaded while the existing ones run overtime.
Operators load the same way each time until a new part arrives, and mistakes in fixture orientation create scrap and crash risk.
When a customer releases a large batch, daily helpers are added quickly and trained by whoever has a moment.
Tool life, offset changes and fixture issues are told in a few words at the gate and lost by the next morning.
When a delivery is late, the quality check is seen as the delay, and inspectors feel pushed to pass doubtful parts.
Cleaning and burr removal are the last step before dispatch and carry high risk of rejection, yet they get little training.
Start with the topics that matter most here: Recruitment and Talent Acquisition; Learning and Development; Onboarding and Probation. Then work through the rest. Each topic is written for manufacturing, not in general.
Requisition to joining, the same way every time.
Training planned from need rather than from the calendar.
A first day that is the same for the fifth joiner as the first.
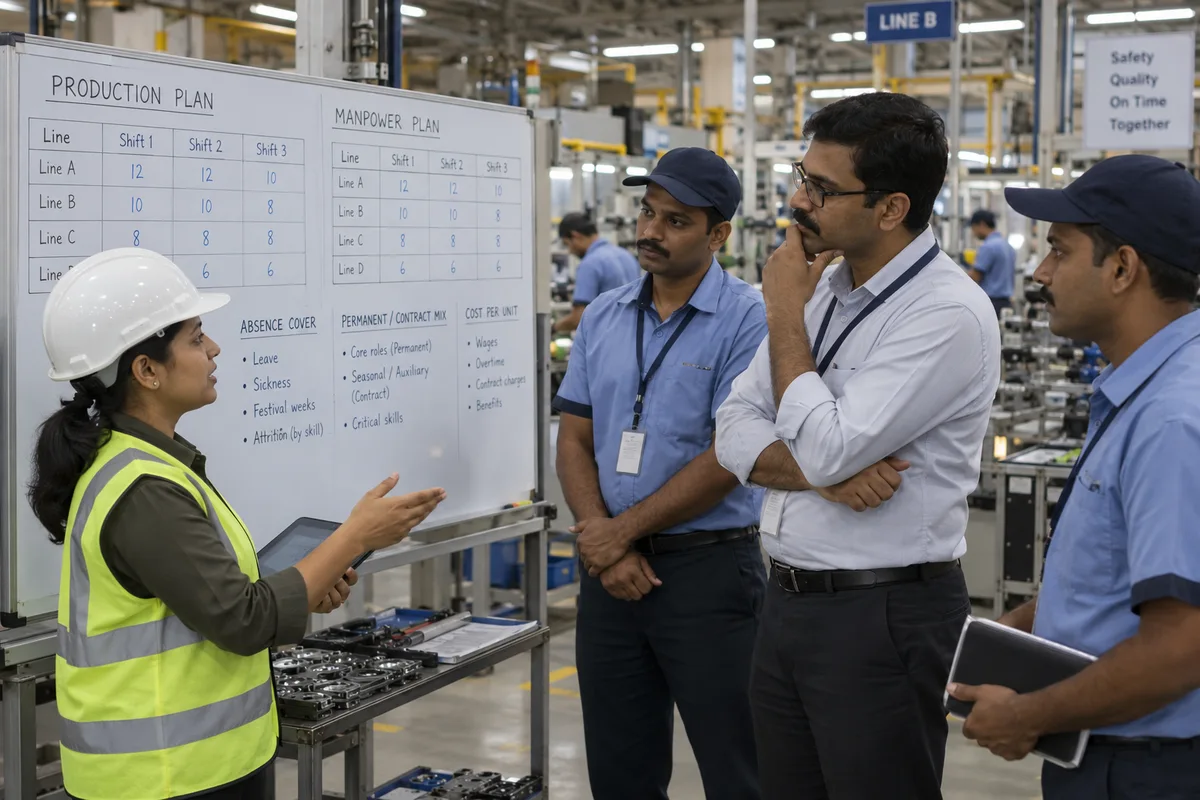
How many people, in which roles, by when — and what they will cost.
Structure, reporting lines and who is allowed to decide what.
Records, attendance, leave and the day-to-day HR that must simply work.
Salary structure, payroll inputs and a month that closes on time.
Goals, reviews and ratings that hold up in a conversation.
Named backups for the roles that cannot be vacant.
Communication, recognition and the conditions people actually work in.
Two routes — one for complaints, one for conduct — kept separate.
Policies a manager can apply, and obligations with owners and dates.
Induction, records, incident reporting and follow-through.
Who leaves, when, why — and which of them mattered.
Resignation to relieving letter, in a defined order.
Records that survive people, and approvals that do not queue.
A short monthly pack management actually reads.
An HR function that runs the same way every month.
The pieces a VMC machining units business puts in place, in an order that makes each easier. Open any card for the detail.
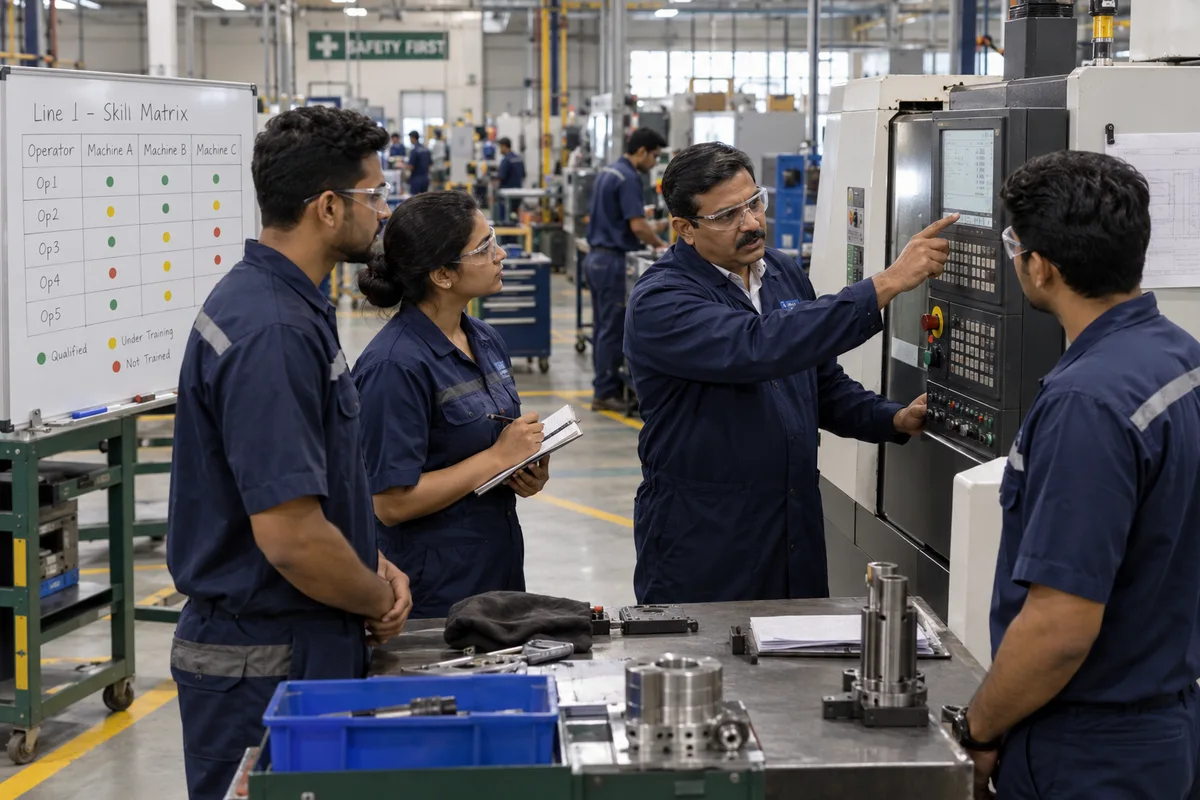
Choose and train two operators for each planned machine, using a staged list of setter tasks.
What this coversHideChoose and train two operators for each planned machine, using a staged list of setter tasks. A recruitment plan can fill gaps from outside where needed.
One page per machine: part, tools near end of life, offsets changed, fixture issues and quality alerts.
What this coversHideOne page per machine: part, tools near end of life, offsets changed, fixture issues and quality alerts. See how the shift and attendance process can include it.
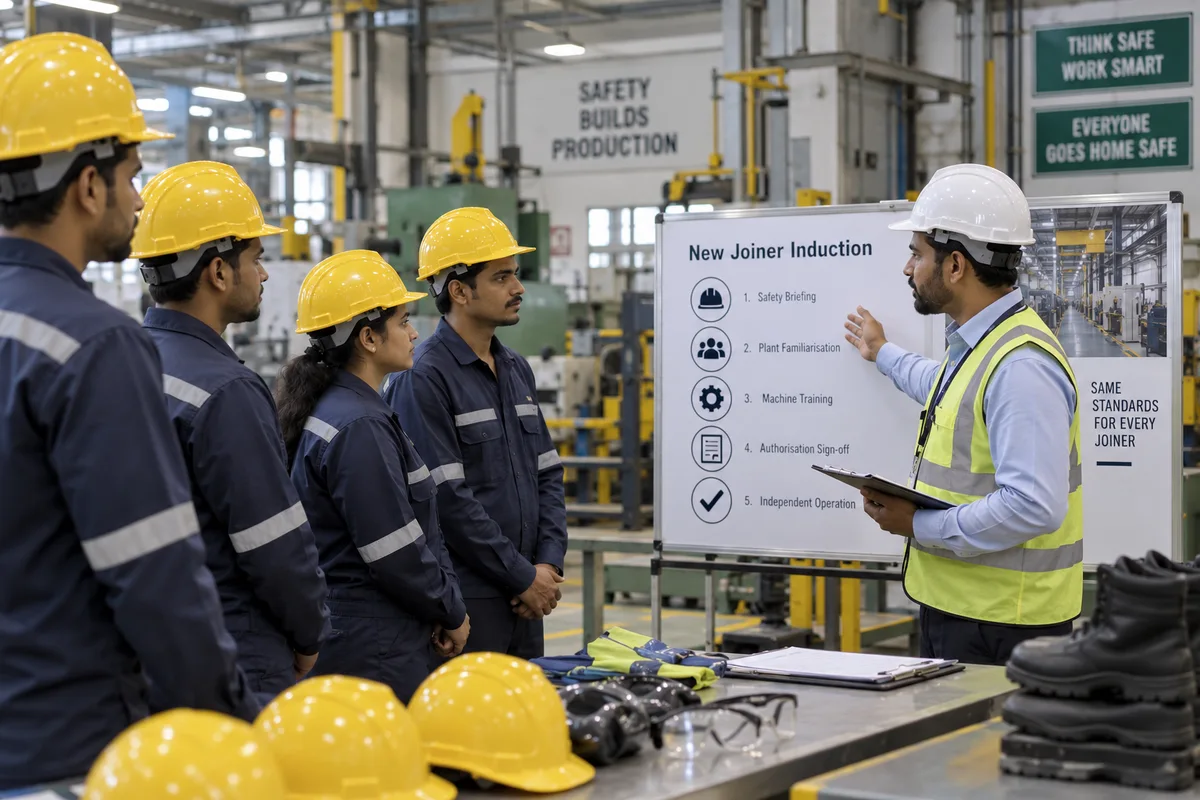
A half-day on safety, part handling, burr limits and who to call, with a named buddy for the first week.
What this coversHideA half-day on safety, part handling, burr limits and who to call, with a named buddy for the first week. The onboarding process can set this out.
State that an inspector's hold cannot be overridden by production, and that the plant head resolves disputes the same day.
What this coversHideState that an inspector's hold cannot be overridden by production, and that the plant head resolves disputes the same day.
A short skills list for deburring and washing and a rejection feedback loop, so those staff see the effect of their work.
What this coversHideA short skills list for deburring and washing and a rejection feedback loop, so those staff see the effect of their work.
Before changing anything, find out what is true today. These checks take an afternoon and tell you which of the topics above to start with.
Share your requirementsConfirm with a qualified professional. What applies to you depends on your business, your state and your arrangements, and it changes. This page describes practice. It does not state a legal position.
The services below fit this kind of business best. Each starts by recording where you stand, and every later report compares against that. We do not promise outcomes.
Quick, clear induction for helpers added during job-work peaks.
Shift patterns and handover habits that keep all machines loaded without burning people out.
Plans and searches for setters and operators ahead of the next machine, not after it.
A staged route from operator to setter so you grow your own bench.
Start with a free conversation, or see the paid HR Diagnostic.
Understand the business, its workforce, current processes and HR challenges.
Find the missing, weak, inconsistent or person-dependent processes.
Create the structure, processes, policies, SOPs, dashboards and systems needed.
Help HR and department managers actually adopt the new system.
Digitise repetitive and approval-based workflows where it is worth doing.
Track hiring, attendance, employee cost, performance, training and attrition.
Strengthen the people-management system continuously, not once.
From the GullyHR blog: one on HR in manufacturing, and one on each of the topics this page points to.
Operators, technicians and supervisors leave for reasons that sit in shifts, skills and supervision. How to ask, read the pattern by shift and act on it.
6 min readRead article
Candidates who accept and never arrive are usually lost in the silence between offer and joining. What actually causes it, and a contact plan that closes the gap.
8 min readRead article
A calendar of courses, a budget spent by March and no record of what any of it changed. What a learning and development process contains when it starts from need rather than from the catalogue.
7 min readRead article
A practical joining checklist covering documents, assets, system access and statutory enrolments, with owners and timings, so nobody's first salary is wrong.
8 min readRead articleMore on the GullyHR blog.
There is no fixed ratio. Look at how many changeovers you do in a shift and how long each takes, then plan a bench so that the absence of one setter does not stop the line.
Usually both. Hire when you need someone immediately and train from within so people see a future. Pay differences between the two groups need careful handling.
Keep a list of reliable part-time or daily workers, train them in the basics before they are needed and agree overtime early. Check employment arrangements with a qualified professional.
The part running, tools close to change, offsets altered, fixture or quality alerts and anything that needs the setter's attention. Keep it to one page.
Make clear in writing that a hold can only be lifted by the plant head, and review each override. Praise inspectors whose catches saved a customer return.
We would count setters against machines, read your shift handover practice and ask how job-work helpers are inducted. A good first piece of work is a setter bench plan with a handover sheet. Scope is agreed in writing afterwards.
All 9 business types in CNC machining and precision engineering · Find another business type
Identify payroll leaks, record gaps and hiring bottlenecks in a free first conversation, and leave knowing what to fix first.
Know what you need? Share your requirements in four short steps.
Want the full picture? See the paid HR Diagnostic.
Prefer a quick message? Chat on WhatsApp