
Industries
Why manufacturing employees leave and how to understand why
Operators, technicians and supervisors leave for reasons that sit in shifts, skills and supervision. How to ask, read the pattern by shift and act on it.
6 min readRead articleGravity die casting units pour aluminium or brass into steel dies by hand or on tilt machines to make pump, valve and automotive parts. Pour feel, die care and finishing decide quality, and these are learnt by doing, not by a manual.

Not sure what you need? Tell us about your business in six short steps and we will come to the first meeting prepared.
Share your requirementsA gravity die casting unit pours molten aluminium or brass into steel dies without high pressure, using gravity alone, by hand ladle or on tilting machines. Dies are coated, preheated, closed, filled, cooled and opened, and cores may be placed by hand. Cycle times are longer than in pressure die casting, so the pourer's skill with speed, angle and temperature shapes the part. Fettling, shot blasting, heat treatment, leak testing and machining often follow. Many units are family run, serve valve, pump, cookware and auto customers, and rely on a small group of pourers and die care staff who know the dies by touch. See also HR for manufacturing.
These are the places the people side of this kind of business tends to give way. The rest of this page works through them.
HR here has to work for each of these groups, not only the office. The set-up below is written with all of them in mind.
The angle, speed and temperature of a pour are learnt by repetition, and new pourers produce rejects for months before they settle.
Poor coating or uneven preheat wears dies and spoils parts, yet the helper who does it is the least trained person on the floor.
Standing at a die in summer, with molten metal at hand, leads to fatigue and mistakes late in the shift.
Parts that come off the die with flash or porosity pile up at fettling, and the crew absorbs the cost of upstream faults.
Machining units find porosity on the cut face and send lots back, and the foundry cannot tell which pourer or shift made them.
Long-serving pourers expect first choice of dies and shifts, and younger staff feel stuck behind them.
Start with the topics that matter most here: Learning and Development; Organisation Design; Performance Management. Then work through the rest. Each topic is written for manufacturing, not in general.
Training planned from need rather than from the calendar.
Structure, reporting lines and who is allowed to decide what.
Goals, reviews and ratings that hold up in a conversation.
How many people, in which roles, by when — and what they will cost.
Requisition to joining, the same way every time.
A first day that is the same for the fifth joiner as the first.
Records, attendance, leave and the day-to-day HR that must simply work.
Salary structure, payroll inputs and a month that closes on time.
Named backups for the roles that cannot be vacant.
Communication, recognition and the conditions people actually work in.
Two routes — one for complaints, one for conduct — kept separate.
Policies a manager can apply, and obligations with owners and dates.
Induction, records, incident reporting and follow-through.
Who leaves, when, why — and which of them mattered.
Resignation to relieving letter, in a defined order.
Records that survive people, and approvals that do not queue.
A short monthly pack management actually reads.
An HR function that runs the same way every month.
The pieces a gravity die casting units business puts in place, in an order that makes each easier. Open any card for the detail.
A new pourer starts with simple dies, then moves to complex ones with a senior checking, with sign-offs at each step.
What this coversHideA new pourer starts with simple dies, then moves to complex ones with a senior checking, with sign-offs at each step. See learning and development process.
A short course on coating, preheat and wear signs, and a grade that recognises it.
What this coversHideA short course on coating, preheat and wear signs, and a grade that recognises it. The role design and job descriptions work can set it out.
A simple tag or batch mark so returns from machining or customers point to a die, pourer and shift.
What this coversHideA simple tag or batch mark so returns from machining or customers point to a die, pourer and shift. This feeds HR reporting and analytics.
A pattern that gives each pourer breaks, shade or lighter dies in heat, with a handover note on die condition, as part of attendance, shift and leave planning.
What this coversHideA pattern that gives each pourer breaks, shade or lighter dies in heat, with a handover note on die condition, as part of attendance, shift and leave planning.
Rules on who gets which die and shift, based on skill grade and rotation, so seniority is respected and young staff can progress.
What this coversHideRules on who gets which die and shift, based on skill grade and rotation, so seniority is respected and young staff can progress.
Before changing anything, find out what is true today. These checks take an afternoon and tell you which of the topics above to start with.
Share your requirementsConfirm with a qualified professional. What applies to you depends on your business, your state and your arrangements, and it changes. This page describes practice. It does not state a legal position.
The services below fit this kind of business best. Each starts by recording where you stand, and every later report compares against that. We do not promise outcomes.
A step-by-step route for pourers and die care staff so skill is built, not guessed at.
A proper role for die care and a clear grade for pourers, instead of an informal pecking order.
Simple reports on rejects, absence and overtime by shift and die, so decisions use records, not memory.
Rotations and breaks for pourers working in heat, with handover notes between shifts.
Start with a free conversation, or see the paid HR Diagnostic.
Understand the business, its workforce, current processes and HR challenges.
Find the missing, weak, inconsistent or person-dependent processes.
Create the structure, processes, policies, SOPs, dashboards and systems needed.
Help HR and department managers actually adopt the new system.
Digitise repetitive and approval-based workflows where it is worth doing.
Track hiring, attendance, employee cost, performance, training and attrition.
Strengthen the people-management system continuously, not once.
From the GullyHR blog: one on HR in manufacturing, and one on each of the topics this page points to.
Operators, technicians and supervisors leave for reasons that sit in shifts, skills and supervision. How to ask, read the pattern by shift and act on it.
6 min readRead article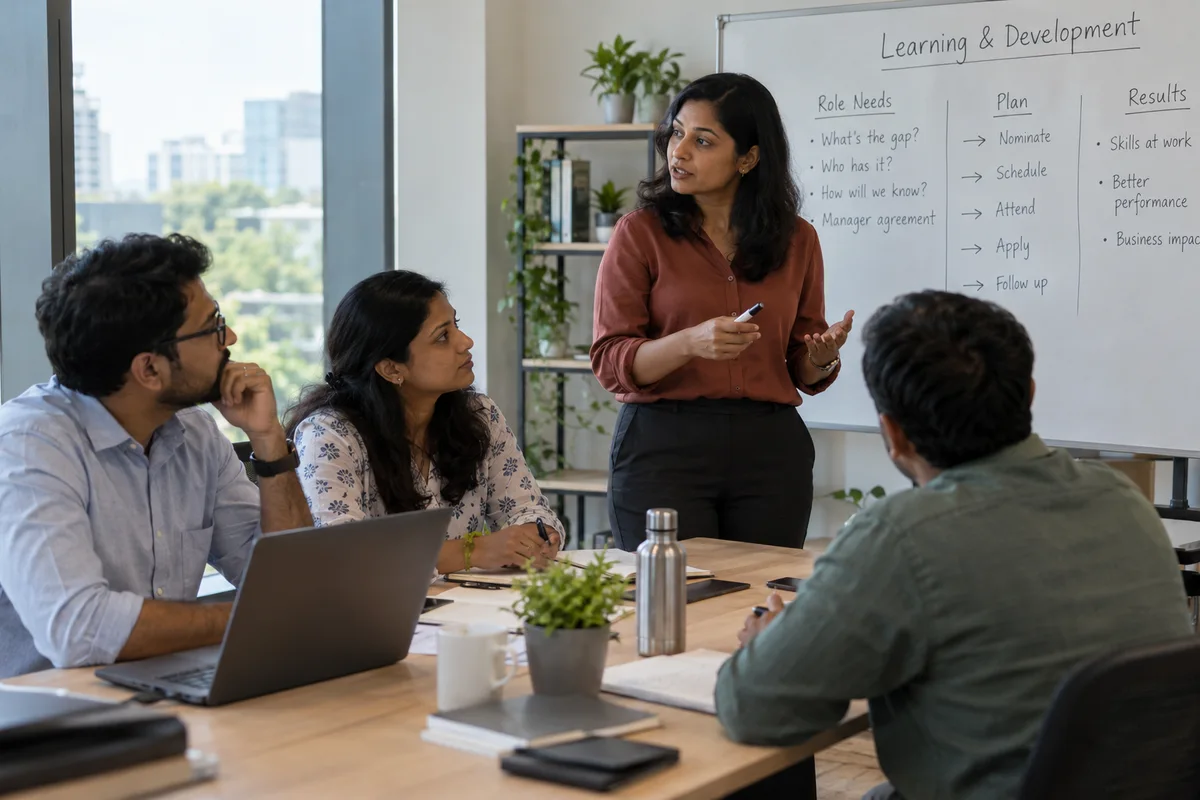
A calendar of courses, a budget spent by March and no record of what any of it changed. What a learning and development process contains when it starts from need rather than from the catalogue.
7 min readRead article
A flat structure works until the founder becomes the only route to a decision. How to tell when you have passed that point, and how to redesign without a reorganisation.
8 min readRead article
A review can only judge what was agreed beforehand. How to set expectations that are specific, written and revisited, so the review stops being a surprise.
5 min readRead articleMore on the GullyHR blog.
It depends on the die, but expect months of supervised work. A step-by-step plan with sign-offs shortens the time and reduces rejects.
Because it is a skill that the least trained person often does. Training and recognising die care staff lowers wear, scrap and downtime.
Mark parts by die, shift and date at the foundry. Then returns can be traced without guessing, and feedback can be fair and specific.
Write rules for die and shift allocation based on skill grade and rotation. Seniors keep respect, and juniors can see how to progress.
Rotate pourers, schedule breaks, keep water close and move hard dies away from the hottest hours where you can. Ask the crew what helps them most.
We would look at which pourers can handle which dies, how die care staff are trained, and whether returns can be traced to a die and shift. A good first piece of work is a pourer skill ladder with a die care role. Scope is agreed in writing afterwards.
All 7 business types in casting and foundry · Find another business type
Identify payroll leaks, record gaps and hiring bottlenecks in a free first conversation, and leave knowing what to fix first.
Know what you need? Share your requirements in four short steps.
Want the full picture? See the paid HR Diagnostic.
Prefer a quick message? Chat on WhatsApp